Fluidized Boiler: Efficient Energy Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

fluidized boiler

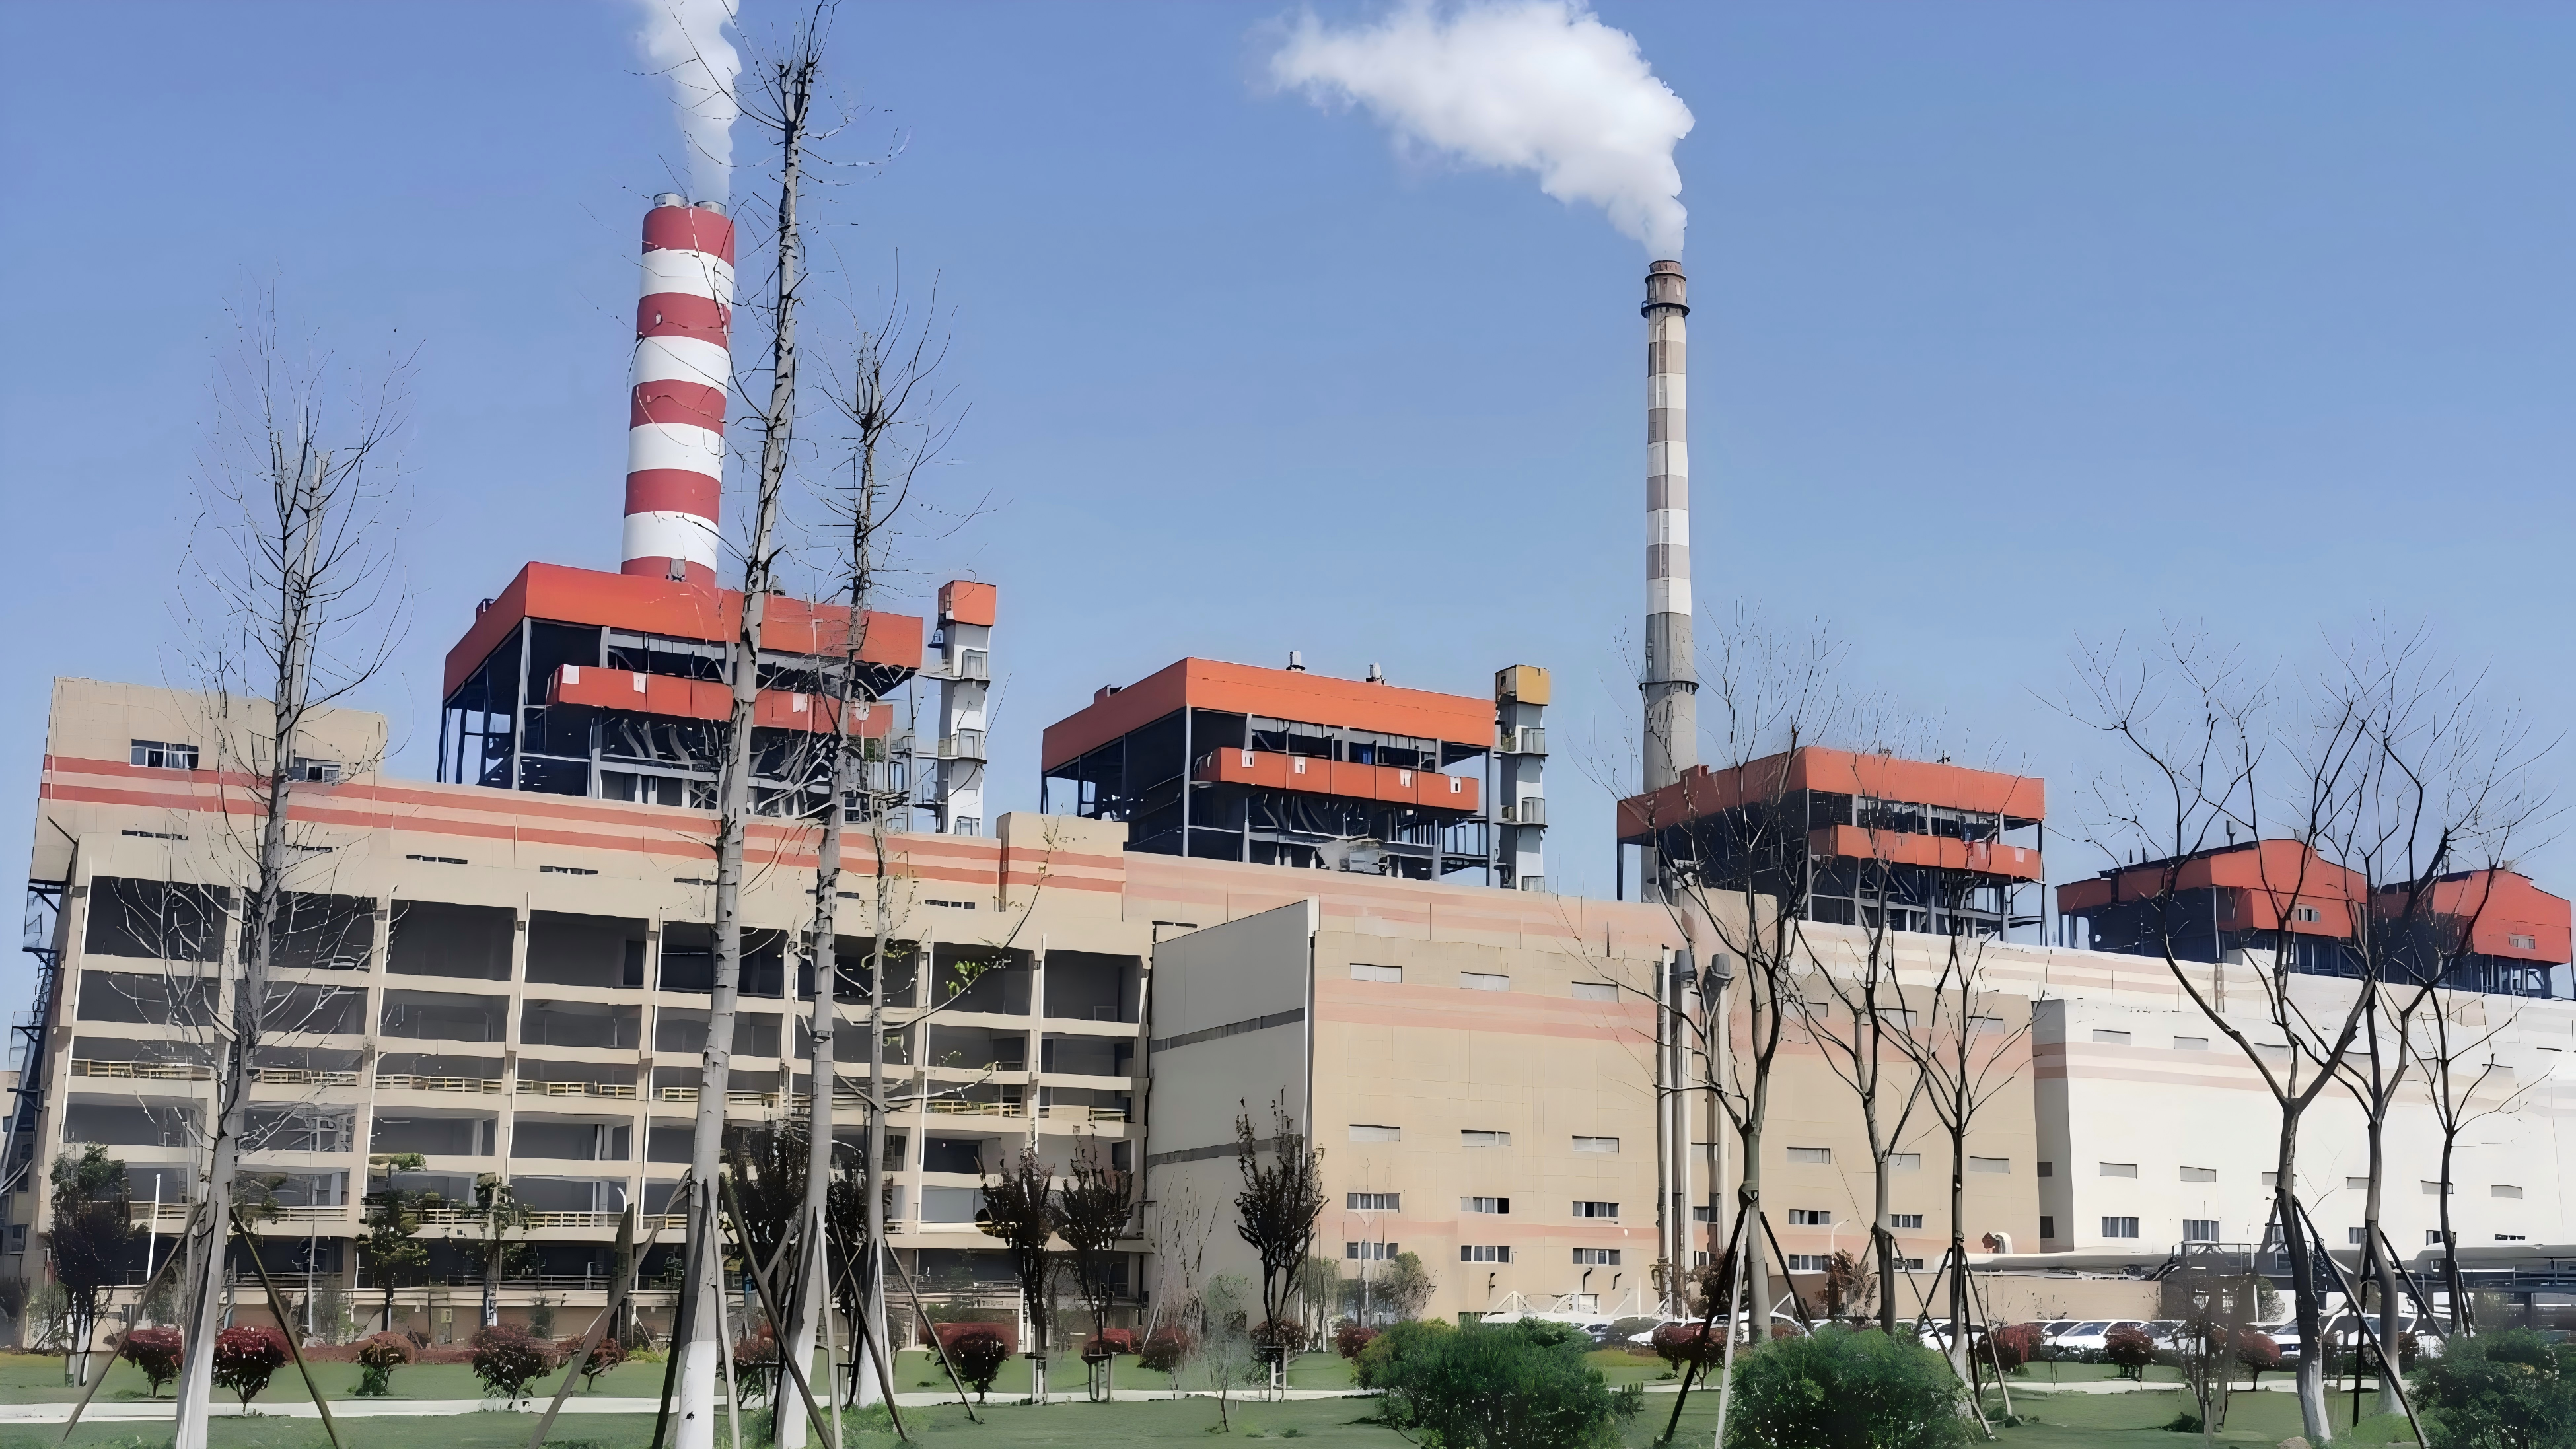
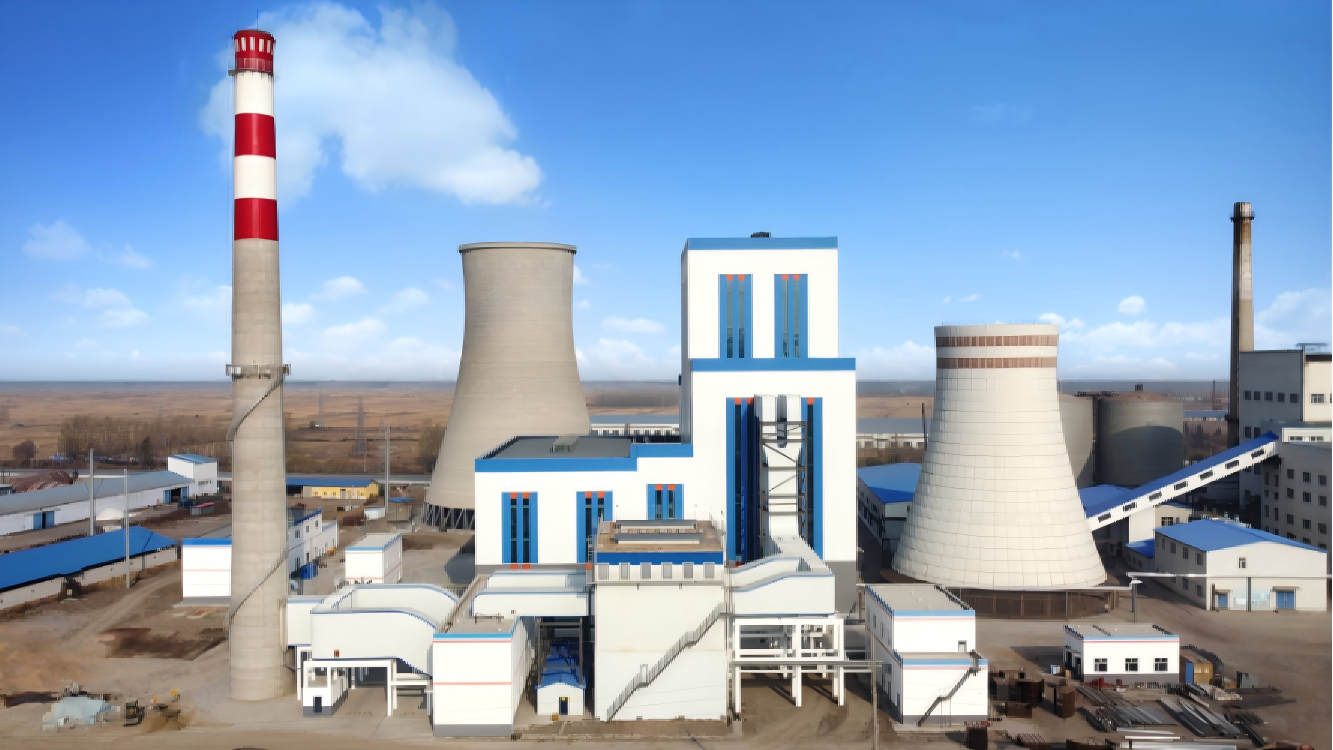
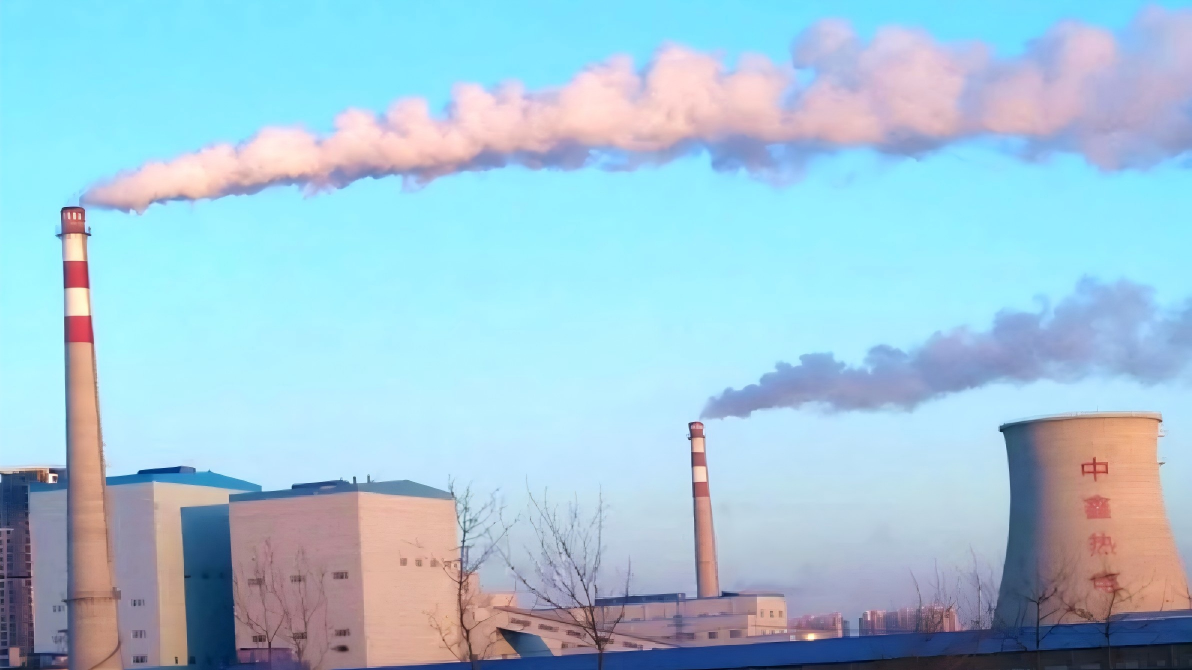
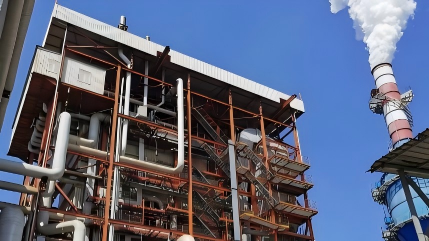
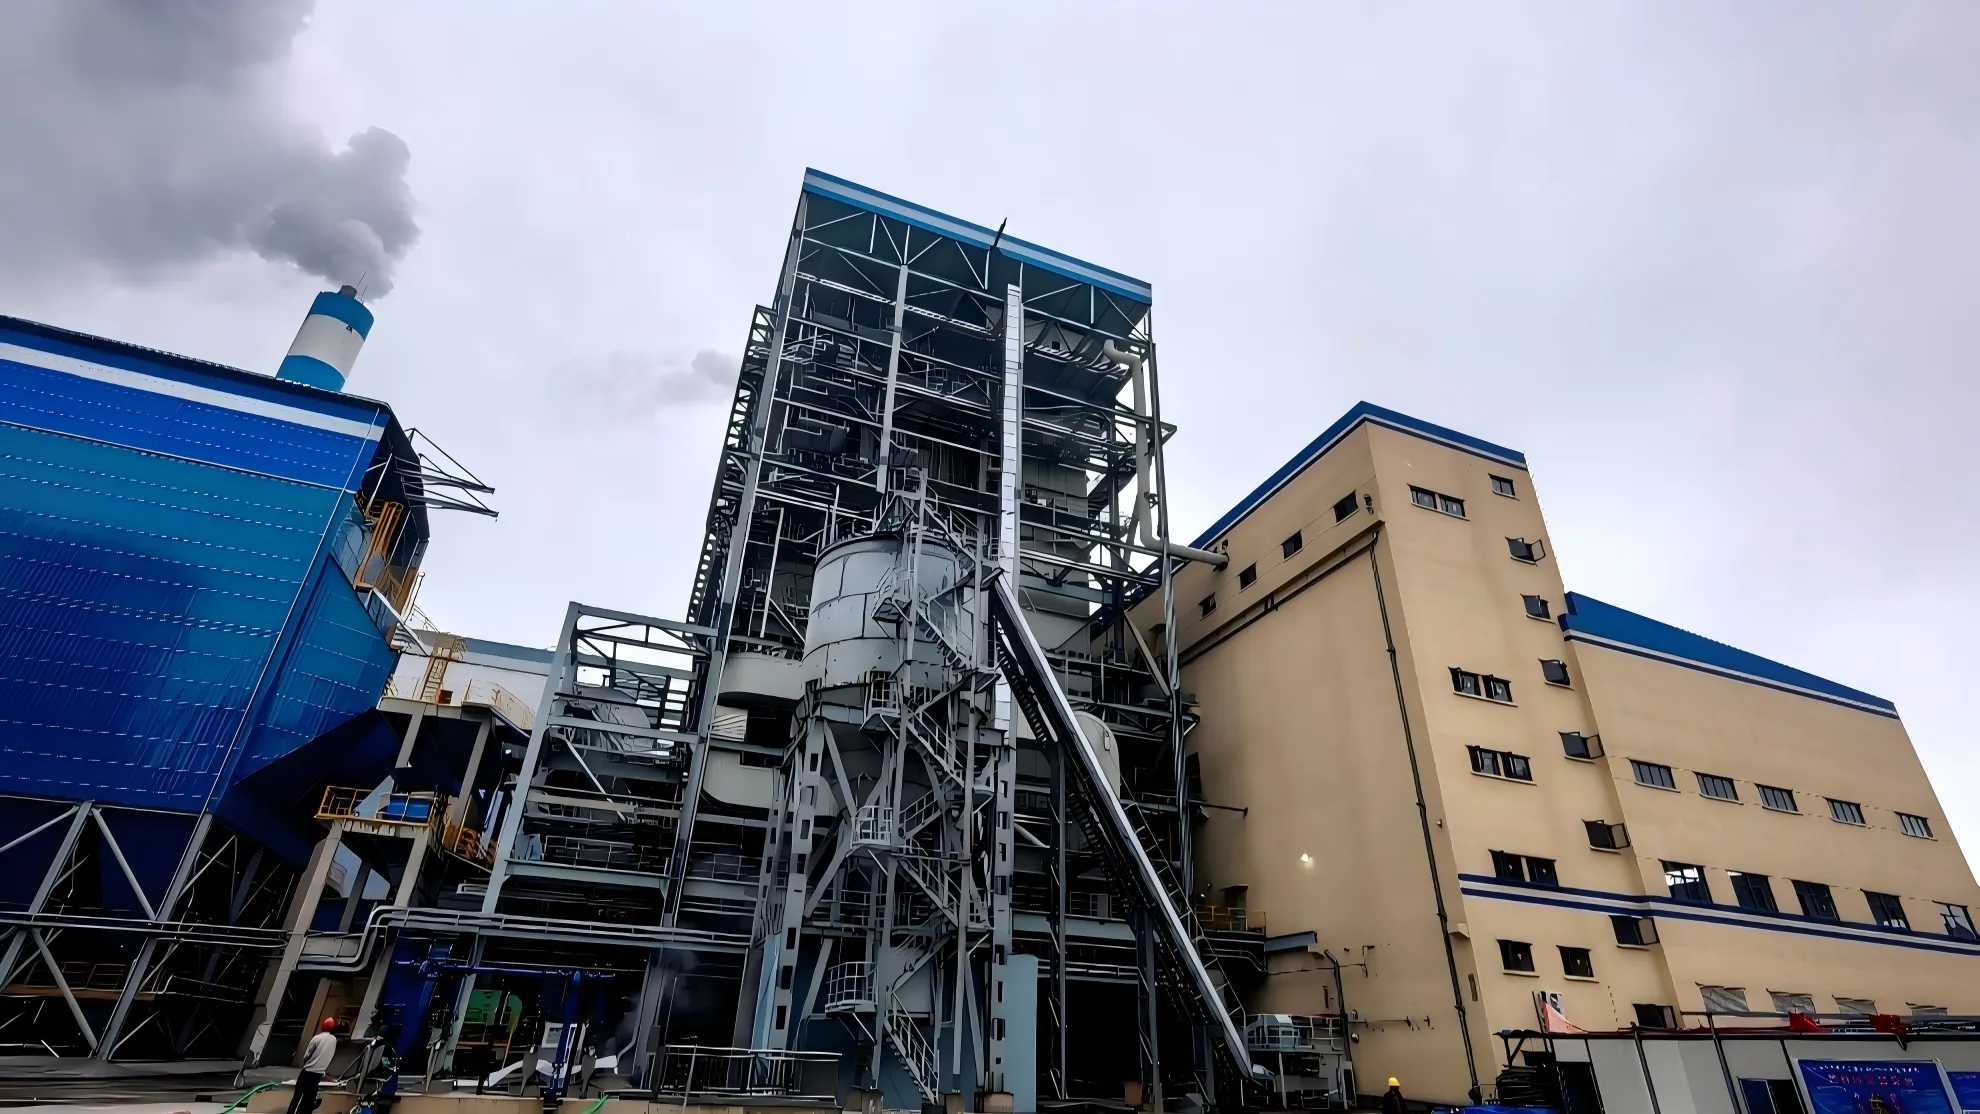
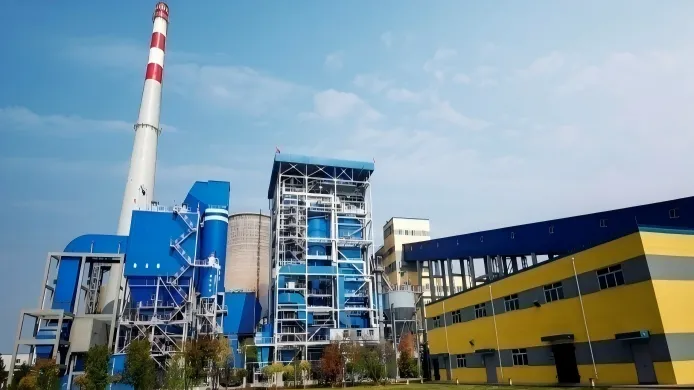
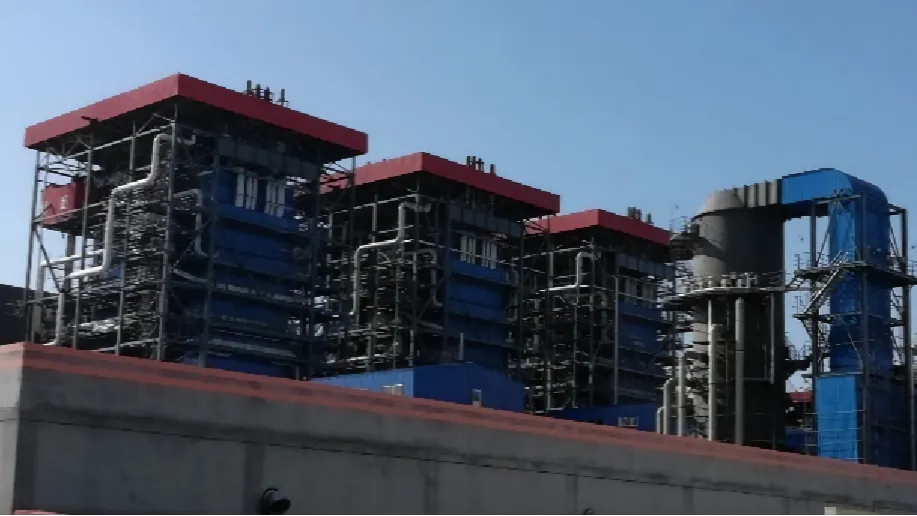
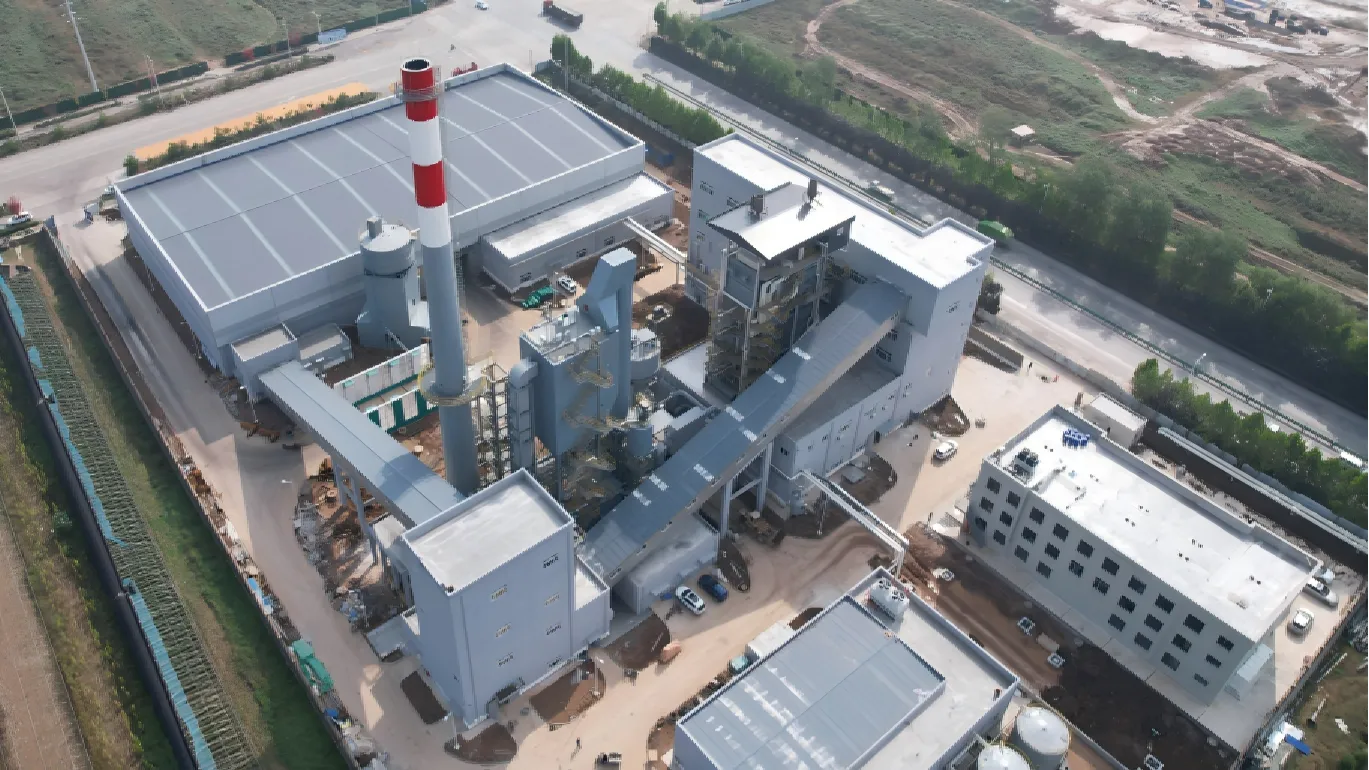
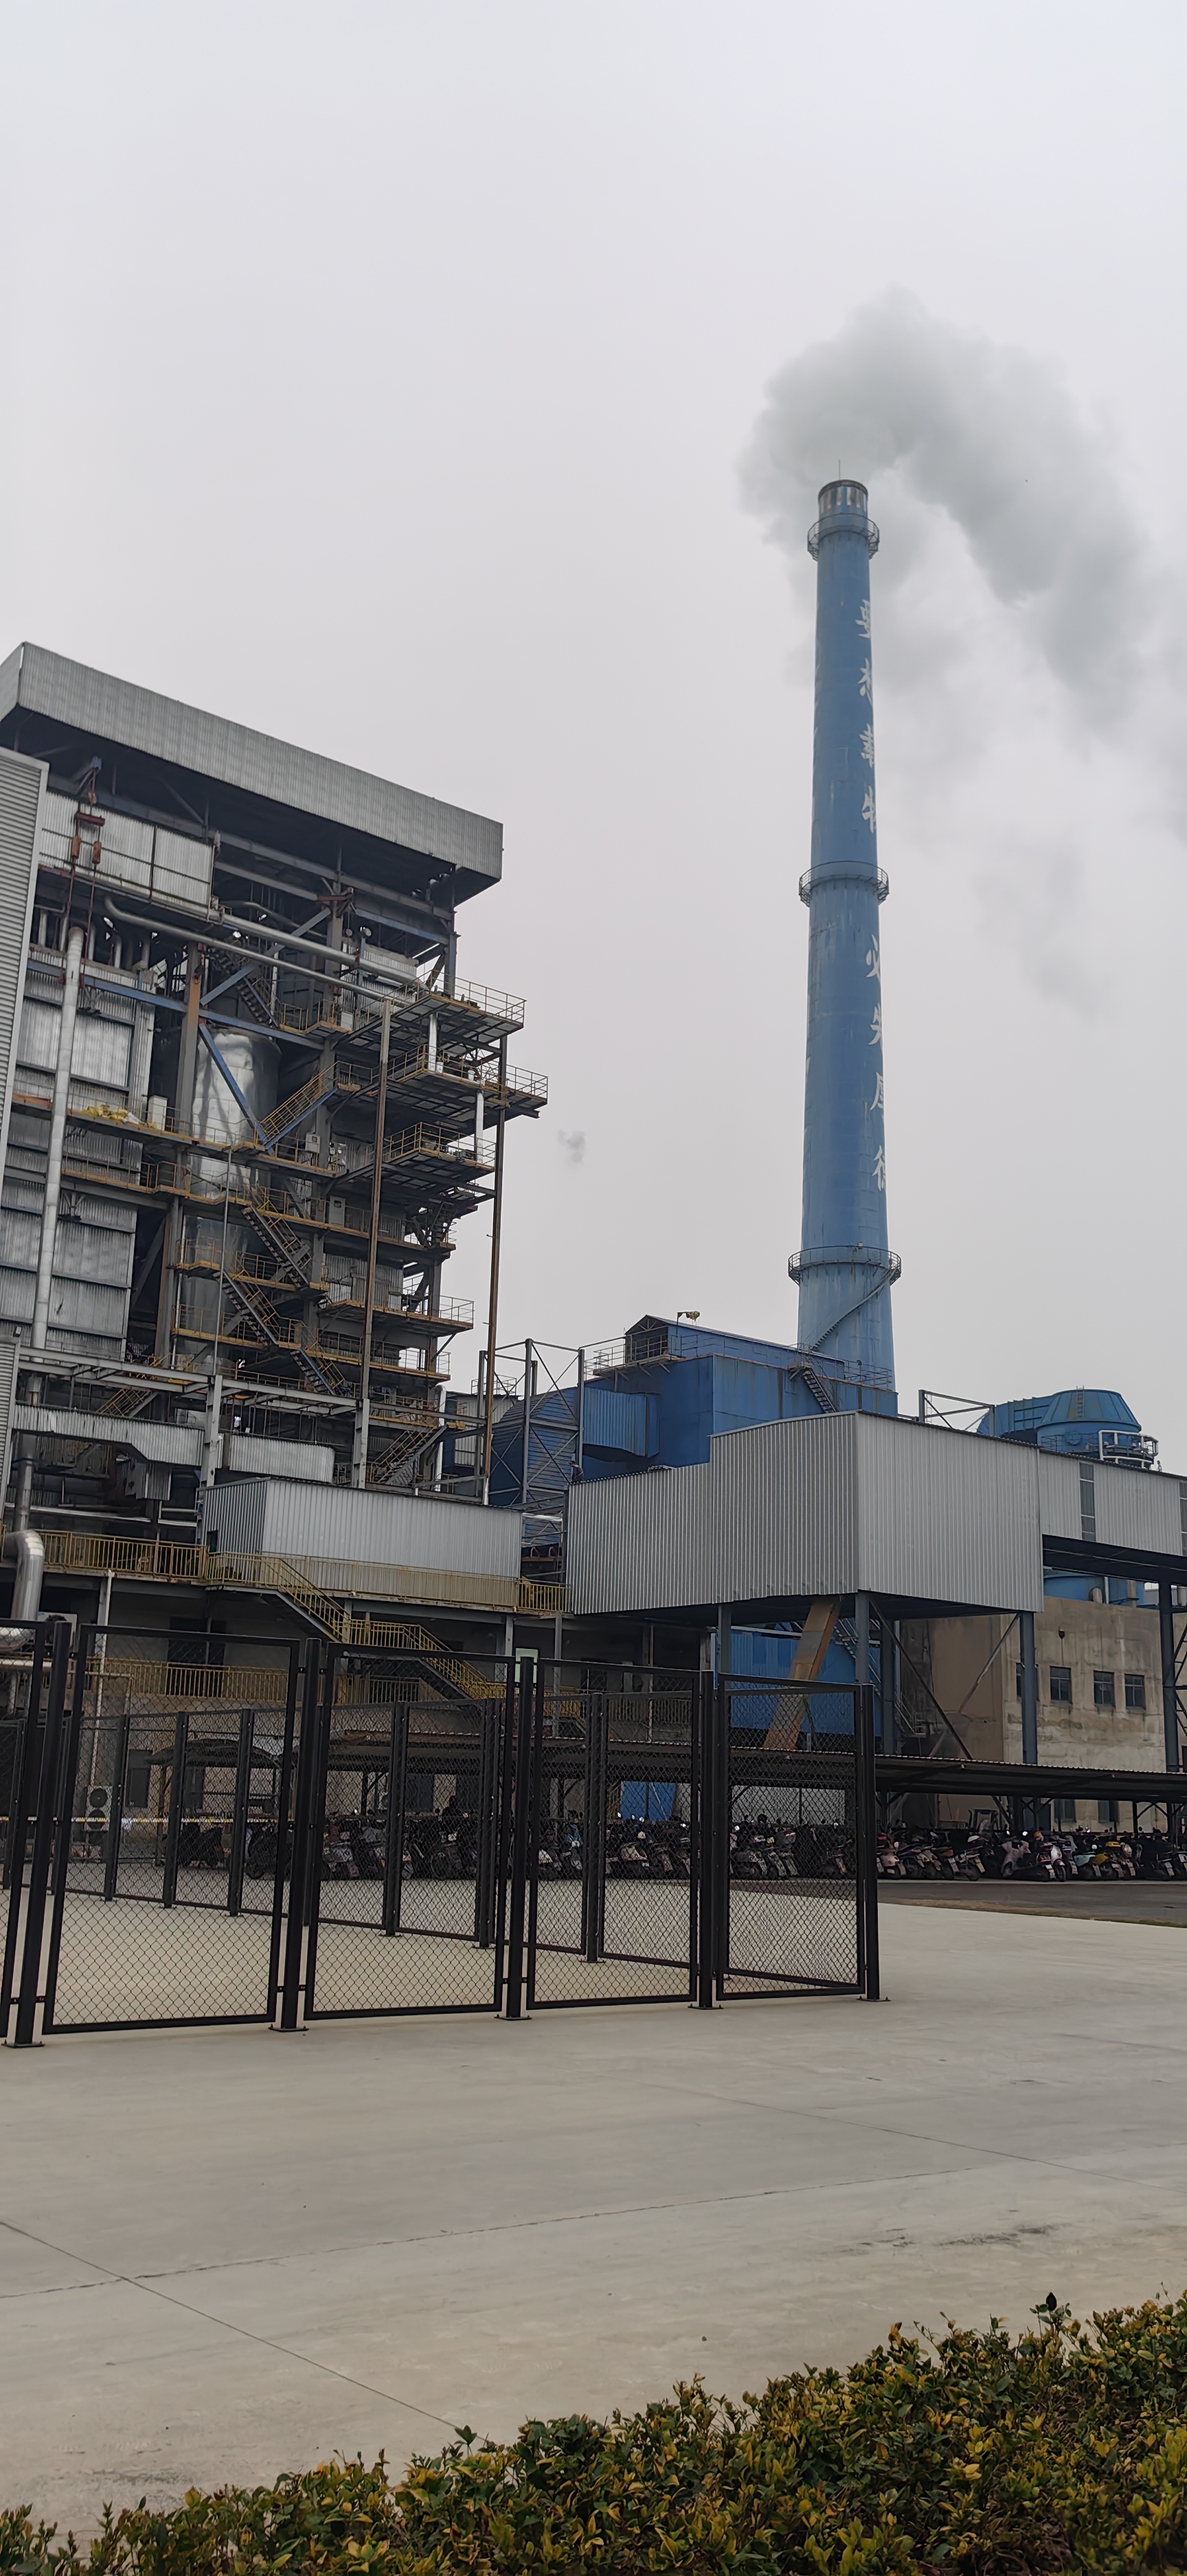
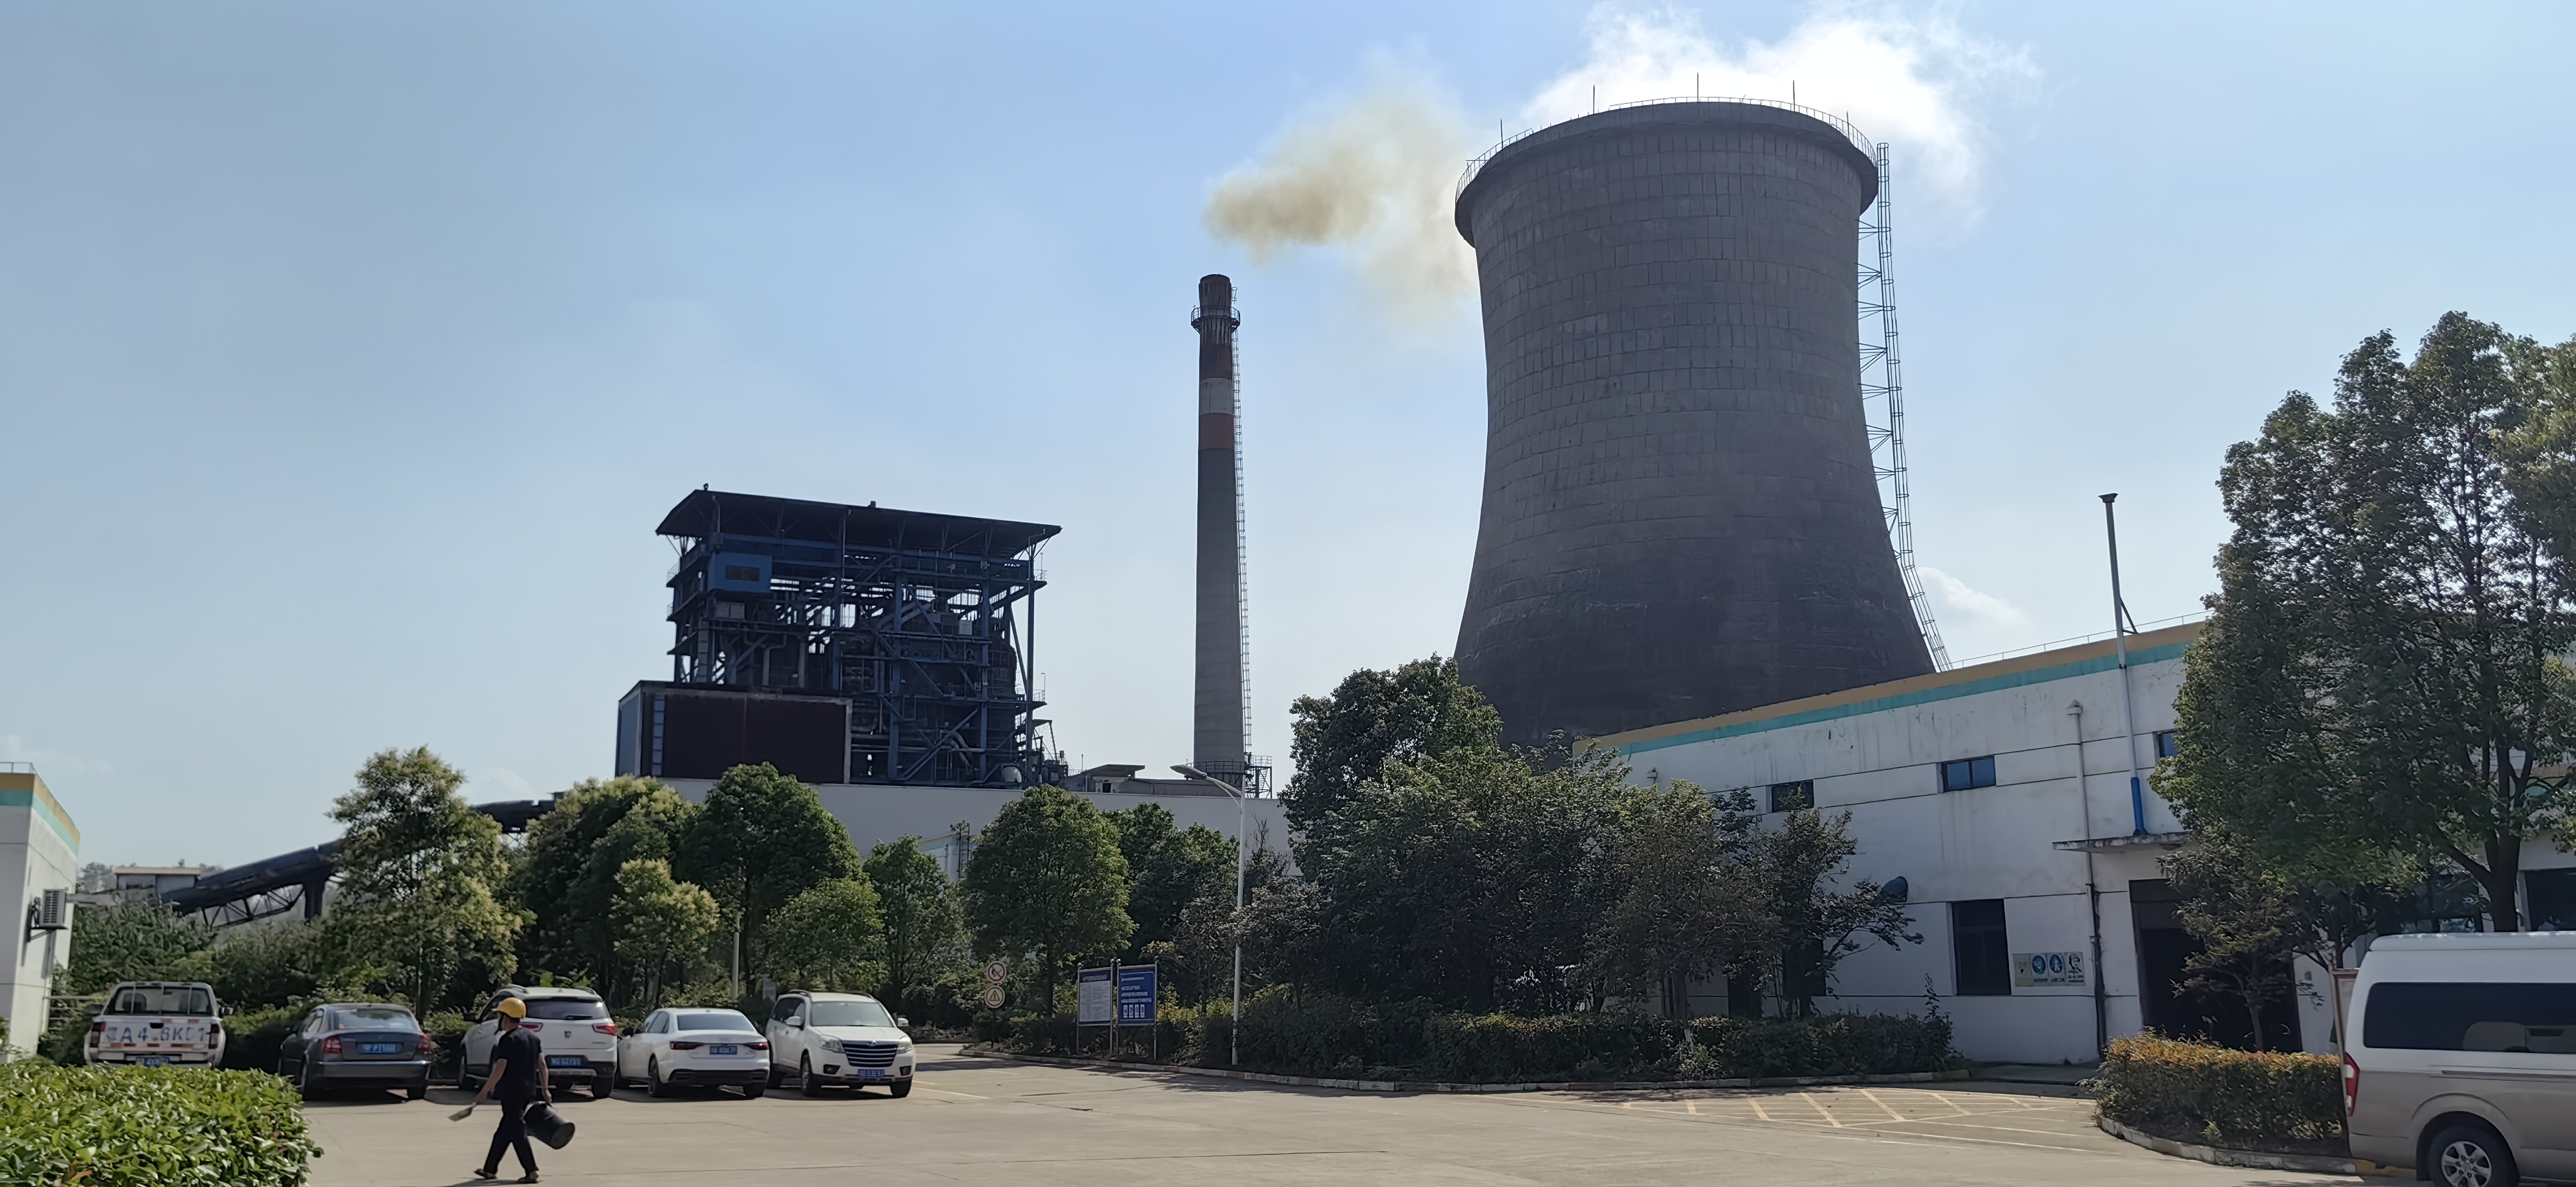
A fluidized boiler represents an advanced combustion technology that revolutionizes how industries generate steam and heat energy. This innovative system operates by suspending solid fuel particles in a stream of air, creating a dynamic fluidized bed where combustion occurs with exceptional efficiency. The fluidized boiler maintains a carefully controlled environment where limestone or other sorbents can be introduced to capture harmful emissions before they escape into the atmosphere. The fluidized boiler technology features several distinctive technological characteristics that set it apart from conventional boiler systems. The combustion chamber operates at relatively lower temperatures, typically between 800 to 900 degrees Celsius, which significantly reduces nitrogen oxide emissions. This temperature control within the fluidized boiler design enables better heat transfer and more complete fuel combustion, maximizing energy output from every unit of fuel consumed. Applications for the fluidized boiler extend across multiple industries, including power generation facilities, industrial heating plants, and waste-to-energy installations. Operators appreciate how a fluidized boiler can handle various fuel types, from coal and biomass to refuse-derived fuels, making it adaptable to diverse operational requirements. The fluidized boiler's ability to process multiple fuel sources while maintaining environmental compliance has made it increasingly popular among facility managers seeking reliable, sustainable combustion solutions for their heating and power generation needs.

New Products

The fluidized boiler delivers substantial operational and financial benefits that make it an intelligent investment for energy-conscious facilities. First, this technology dramatically improves fuel efficiency by achieving more complete combustion compared to traditional boiler systems. The fluidized bed environment ensures intimate contact between fuel particles and oxygen, resulting in higher combustion rates and maximum energy extraction. Facilities using a fluidized boiler experience notably reduced fuel consumption, directly lowering operational costs and improving return on investment. Environmental compliance becomes significantly easier with a fluidized boiler system. The lower operating temperatures and in-situ emission control capabilities mean facilities can meet stringent environmental regulations without expensive external pollution control equipment. The fluidized boiler naturally captures sulfur dioxide through limestone injection, effectively preventing acid rain precursors from entering the atmosphere. This integrated approach protects both operational budgets and environmental integrity. Operational flexibility represents another compelling advantage of the fluidized boiler technology. Unlike conventional systems requiring specific fuel types, a fluidized boiler accommodates coal, biomass, waste materials, and their combinations. This versatility allows facilities to optimize fuel sourcing based on market availability and pricing, enhancing economic performance. Additionally, the fluidized boiler design enables rapid load changes and responsive operation, adapting quickly to fluctuating energy demands. Maintenance costs decrease substantially with a fluidized boiler system due to lower operating temperatures reducing equipment stress and corrosion rates. The design minimizes slagging and fouling issues that plague traditional boilers, extending equipment lifespan and reliability. Facilities choosing a fluidized boiler gain dependable, economical heat generation with minimal downtime and maintenance interruptions.

Tips And Tricks

What are the vital spare parts to stock for a commercial CFB boiler system?

21

Aug

What are the vital spare parts to stock for a commercial CFB boiler system?

A cfb boiler system represents a significant capital investment for industrial power generation and thermal energy production. Whether operating on coal, biomass, or waste fuel, the reliability of your circulating fluidized bed combustion system dire...
View More
Why is a heavy-duty CFB boiler preferred for large cogeneration projects?

01

Sep

Why is a heavy-duty CFB boiler preferred for large cogeneration projects?

Large cogeneration projects demand equipment that can deliver both reliability and efficiency under demanding operational conditions. The choice of boiler technology fundamentally shapes project success, cost structure, and environmental compliance. ...
View More
How to troubleshoot oxygen distribution issues in an industrial CFB boiler?

08

Sep

How to troubleshoot oxygen distribution issues in an industrial CFB boiler?

Oxygen distribution challenges represent one of the most critical operational issues affecting industrial boiler performance and energy efficiency. In a cfb boiler, proper air supply regulation directly impacts combustion quality, fuel consumption ra...
View More
How does a circulating fluidized bed optimize the combustion residence time?

22

Oct

How does a circulating fluidized bed optimize the combustion residence time?

The circulating fluidized bed represents a transformative approach to combustion optimization in industrial power generation. Unlike traditional fixed-bed systems, this technology maintains fuel particles in continuous suspension within the combustio...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

fluidized boiler

Superior Combustion Efficiency and Fuel Flexibility

Superior Combustion Efficiency and Fuel Flexibility

The fluidized boiler excels in converting diverse fuel sources into reliable, consistent energy output. This exceptional capability stems from the fluidized bed technology, which creates optimal mixing conditions between fuel particles and combustion air. Unlike conventional boilers limited to specific fuel types, a fluidized boiler accepts coal, biomass, municipal waste, and industrial byproducts, providing unprecedented operational flexibility. Facilities gain the ability to source fuels opportunistically, selecting options based on market pricing and availability rather than equipment constraints. The fluidized boiler's broad fuel acceptance significantly reduces procurement limitations and costs. Furthermore, this technology achieves combustion efficiency rates exceeding 95 percent, meaning virtually all fuel potential becomes converted to usable heat energy. This exceptional efficiency directly translates to reduced fuel requirements and lower operational expenses for industrial operators. The fluidized boiler represents the optimal choice for facilities seeking maximum fuel flexibility without sacrificing energy performance or equipment reliability.
Advanced Environmental Emission Control

Advanced Environmental Emission Control

Environmental responsibility becomes seamlessly integrated into operations with a fluidized boiler system. The inherent design of a fluidized boiler operates at reduced temperatures between 800-900 degrees Celsius, naturally suppressing nitrogen oxide formation compared to conventional high-temperature combustion systems. This temperature advantage means a fluidized boiler automatically produces cleaner emissions requiring minimal additional treatment. Moreover, limestone injection within the fluidized boiler chamber captures sulfur dioxide during combustion, eliminating the need for expensive external scrubbing systems. This in-situ emission control significantly reduces capital investment in pollution control infrastructure. Facilities utilizing a fluidized boiler achieve compliance with stringent environmental regulations while maintaining competitive operational costs. The fluidized boiler demonstrates how modern combustion technology harmonizes industrial productivity with environmental stewardship, satisfying regulatory requirements and corporate sustainability commitments simultaneously.
Reduced Operational and Maintenance Costs

Reduced Operational and Maintenance Costs

The fluidized boiler delivers compelling economic advantages through lower maintenance requirements and extended equipment lifespan. The moderate operating temperatures within a fluidized boiler design minimize thermal stress on critical components, dramatically reducing corrosion, erosion, and material degradation rates. Facilities operating a fluidized boiler experience fewer unplanned shutdowns and repairs compared to conventional high-temperature boiler systems. The fluidized boiler's efficient combustion also prevents excessive slagging and fouling accumulation, eliminating costly cleaning procedures and associated downtime. Additionally, a fluidized boiler system generates superior heat transfer characteristics, requiring less fuel to achieve target steam or hot water temperatures. This efficiency advantage compounds over years of operation, delivering substantial cumulative cost savings. Facility managers choosing a fluidized boiler benefit from improved profitability through reduced maintenance labor, fewer replacement parts, minimal emergency repairs, and optimized fuel consumption rates throughout the equipment's operational lifetime.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
email goToTop