Industrial Boiler Manufacturer Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial boiler manufacturer

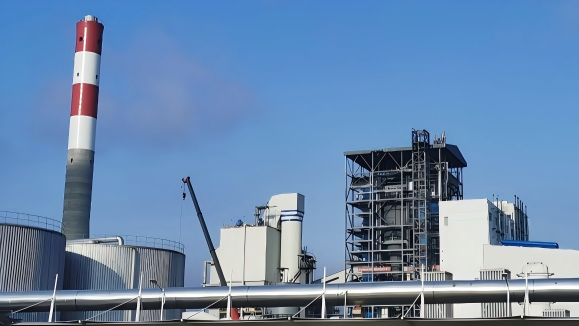
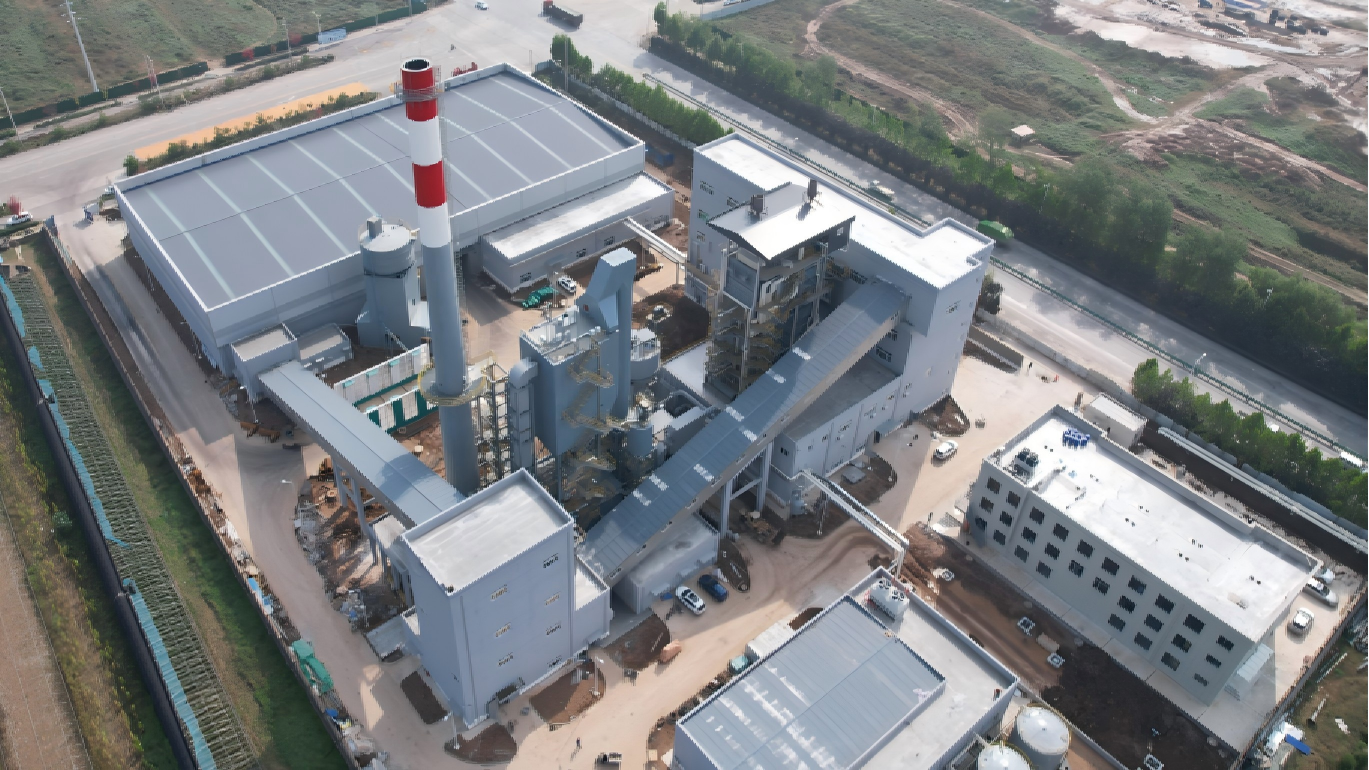
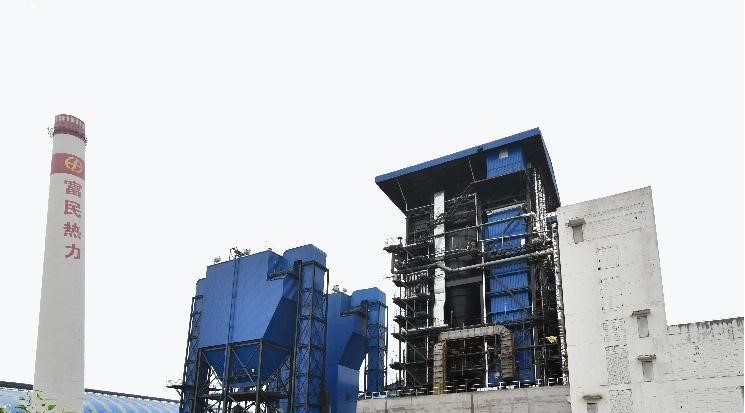
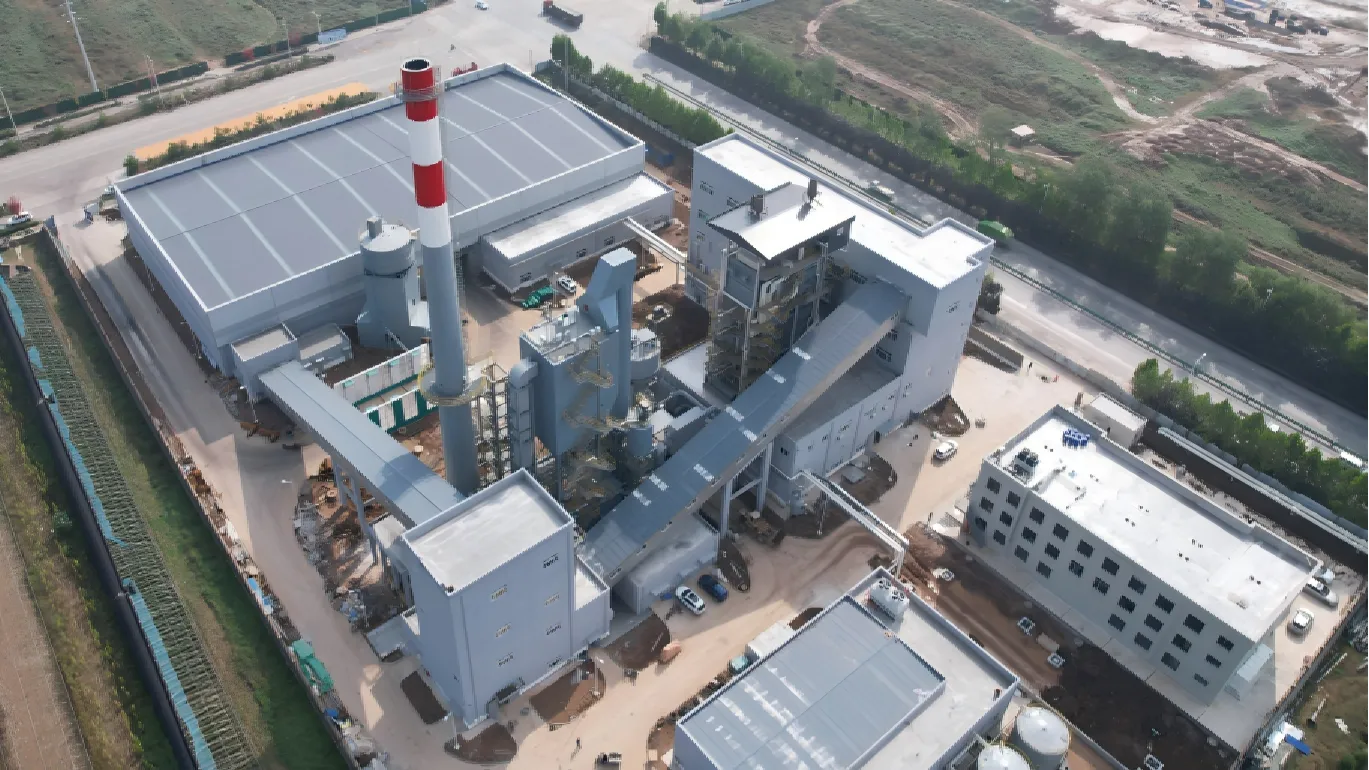
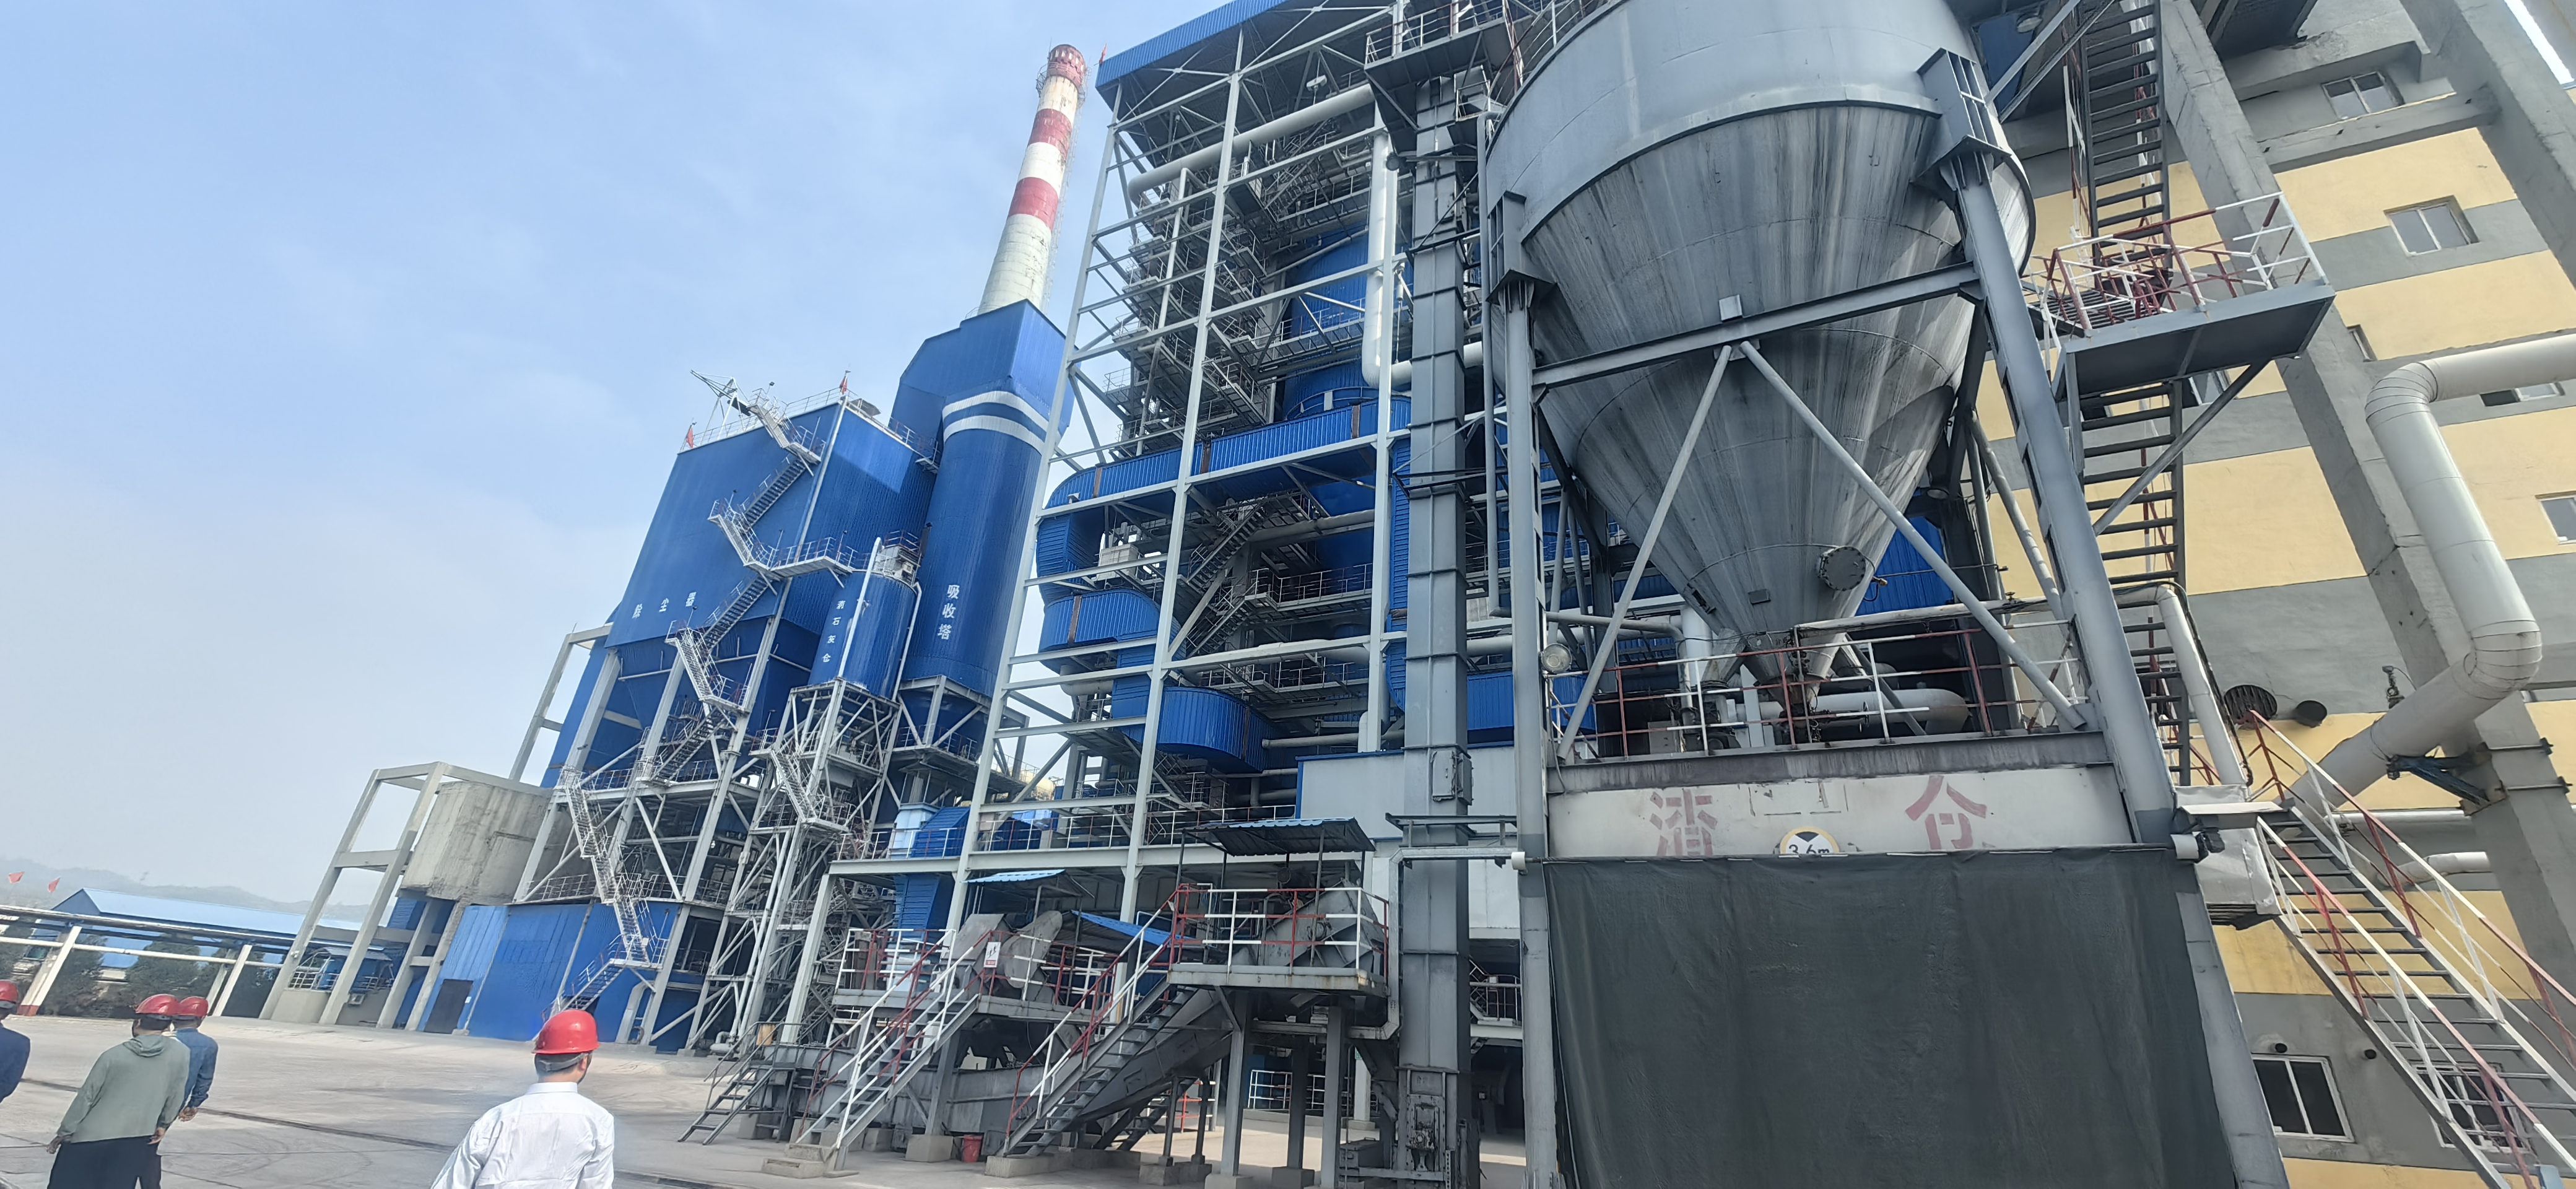
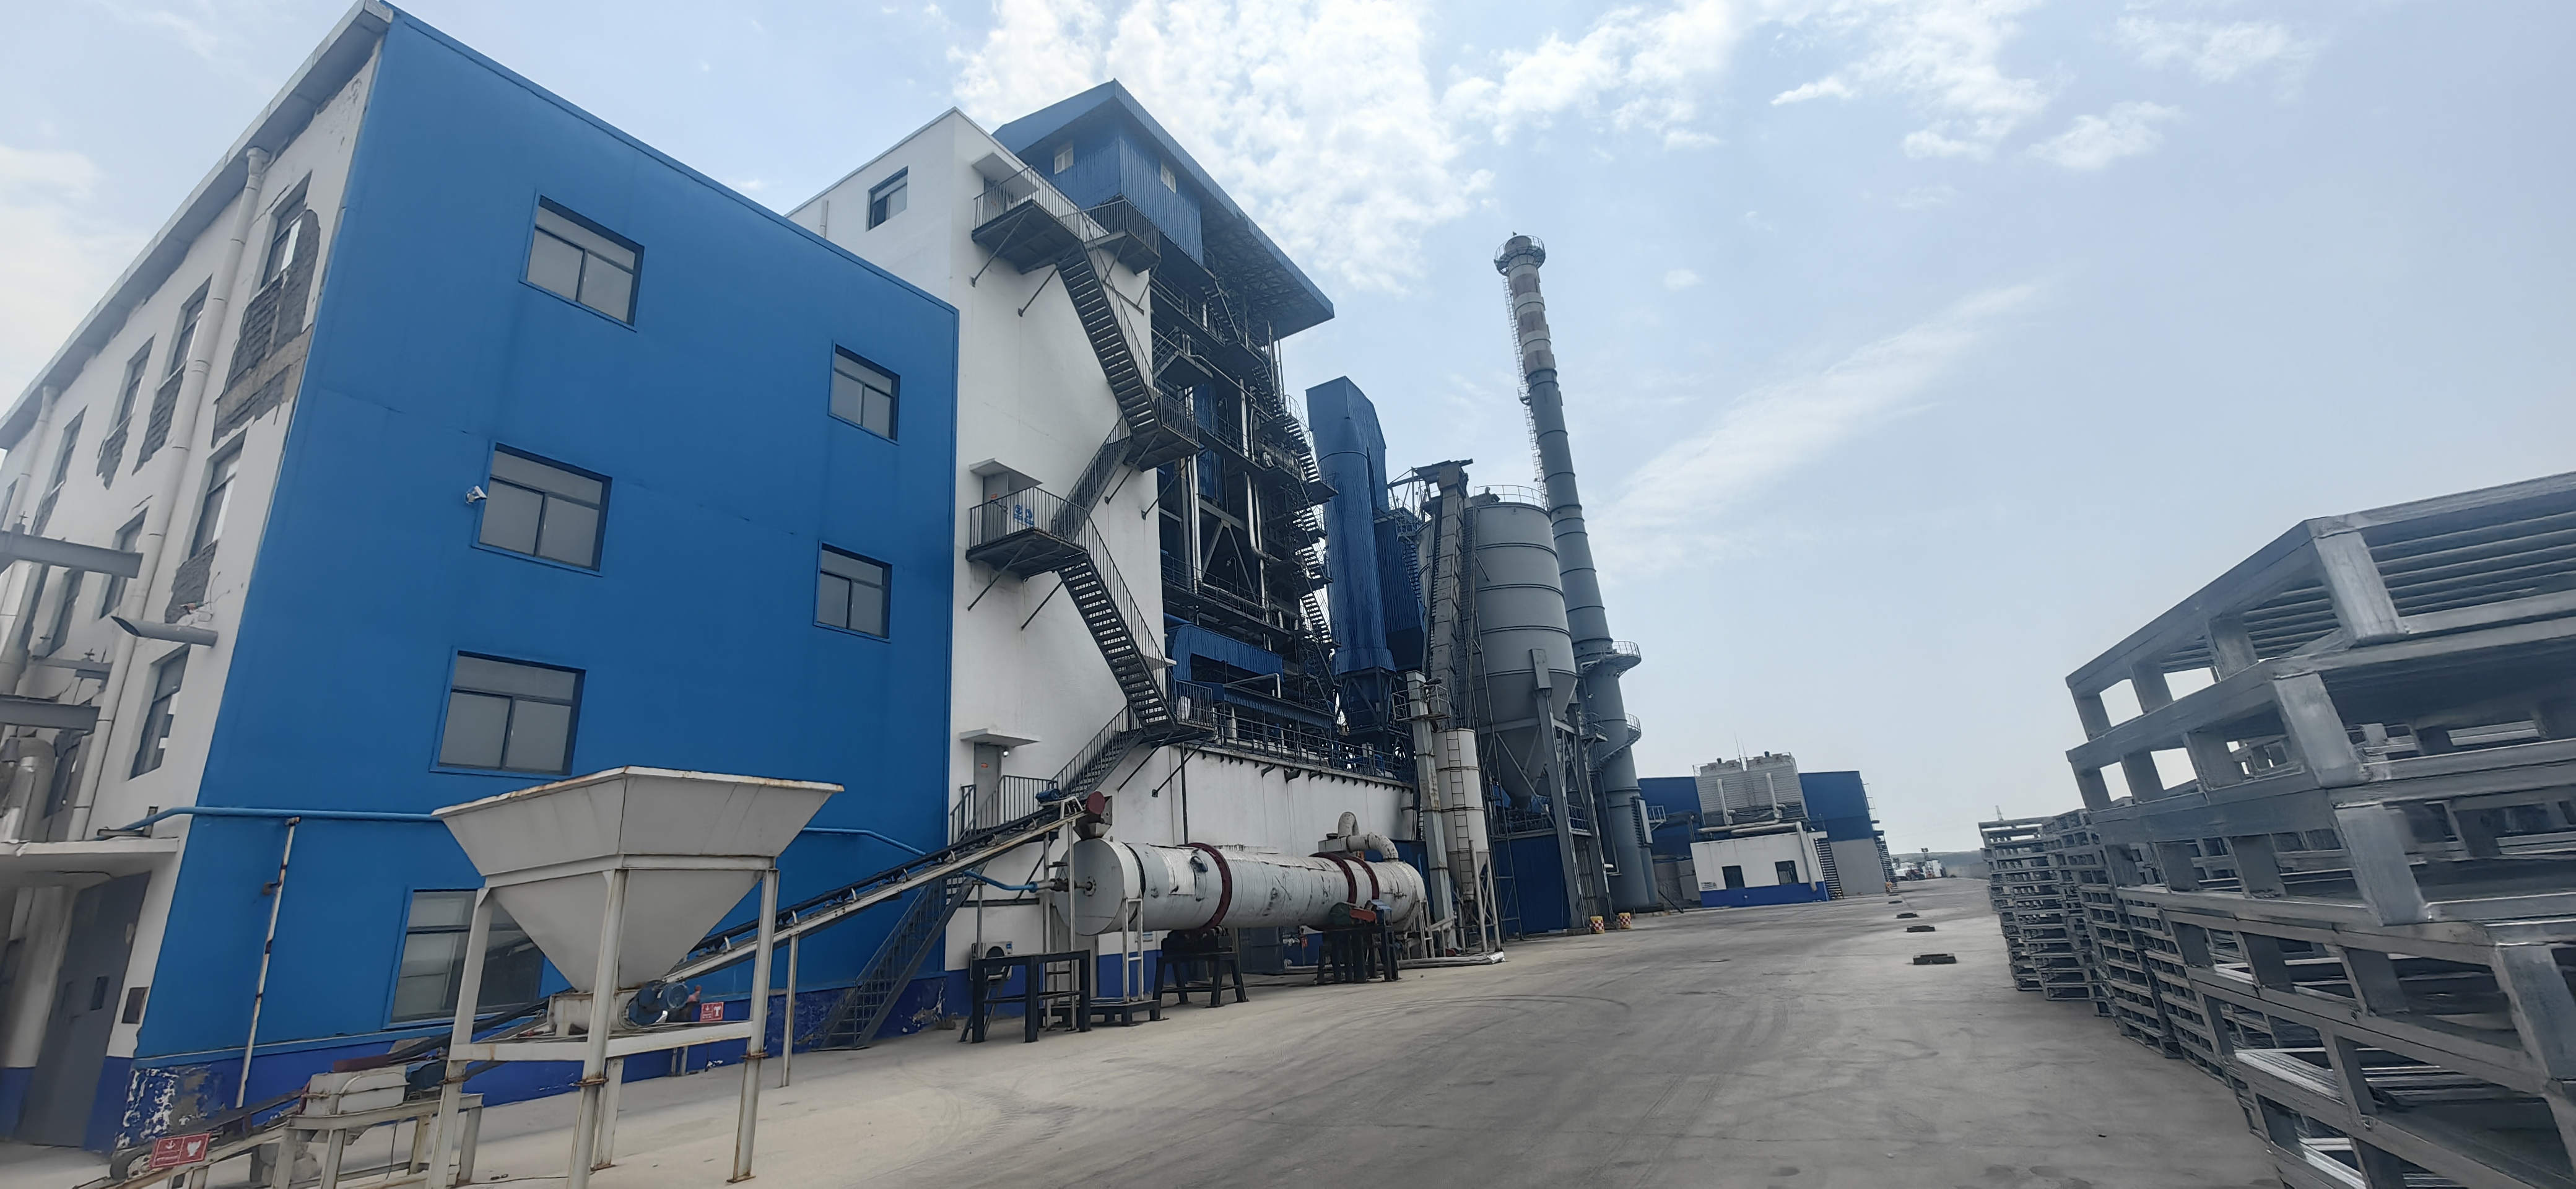
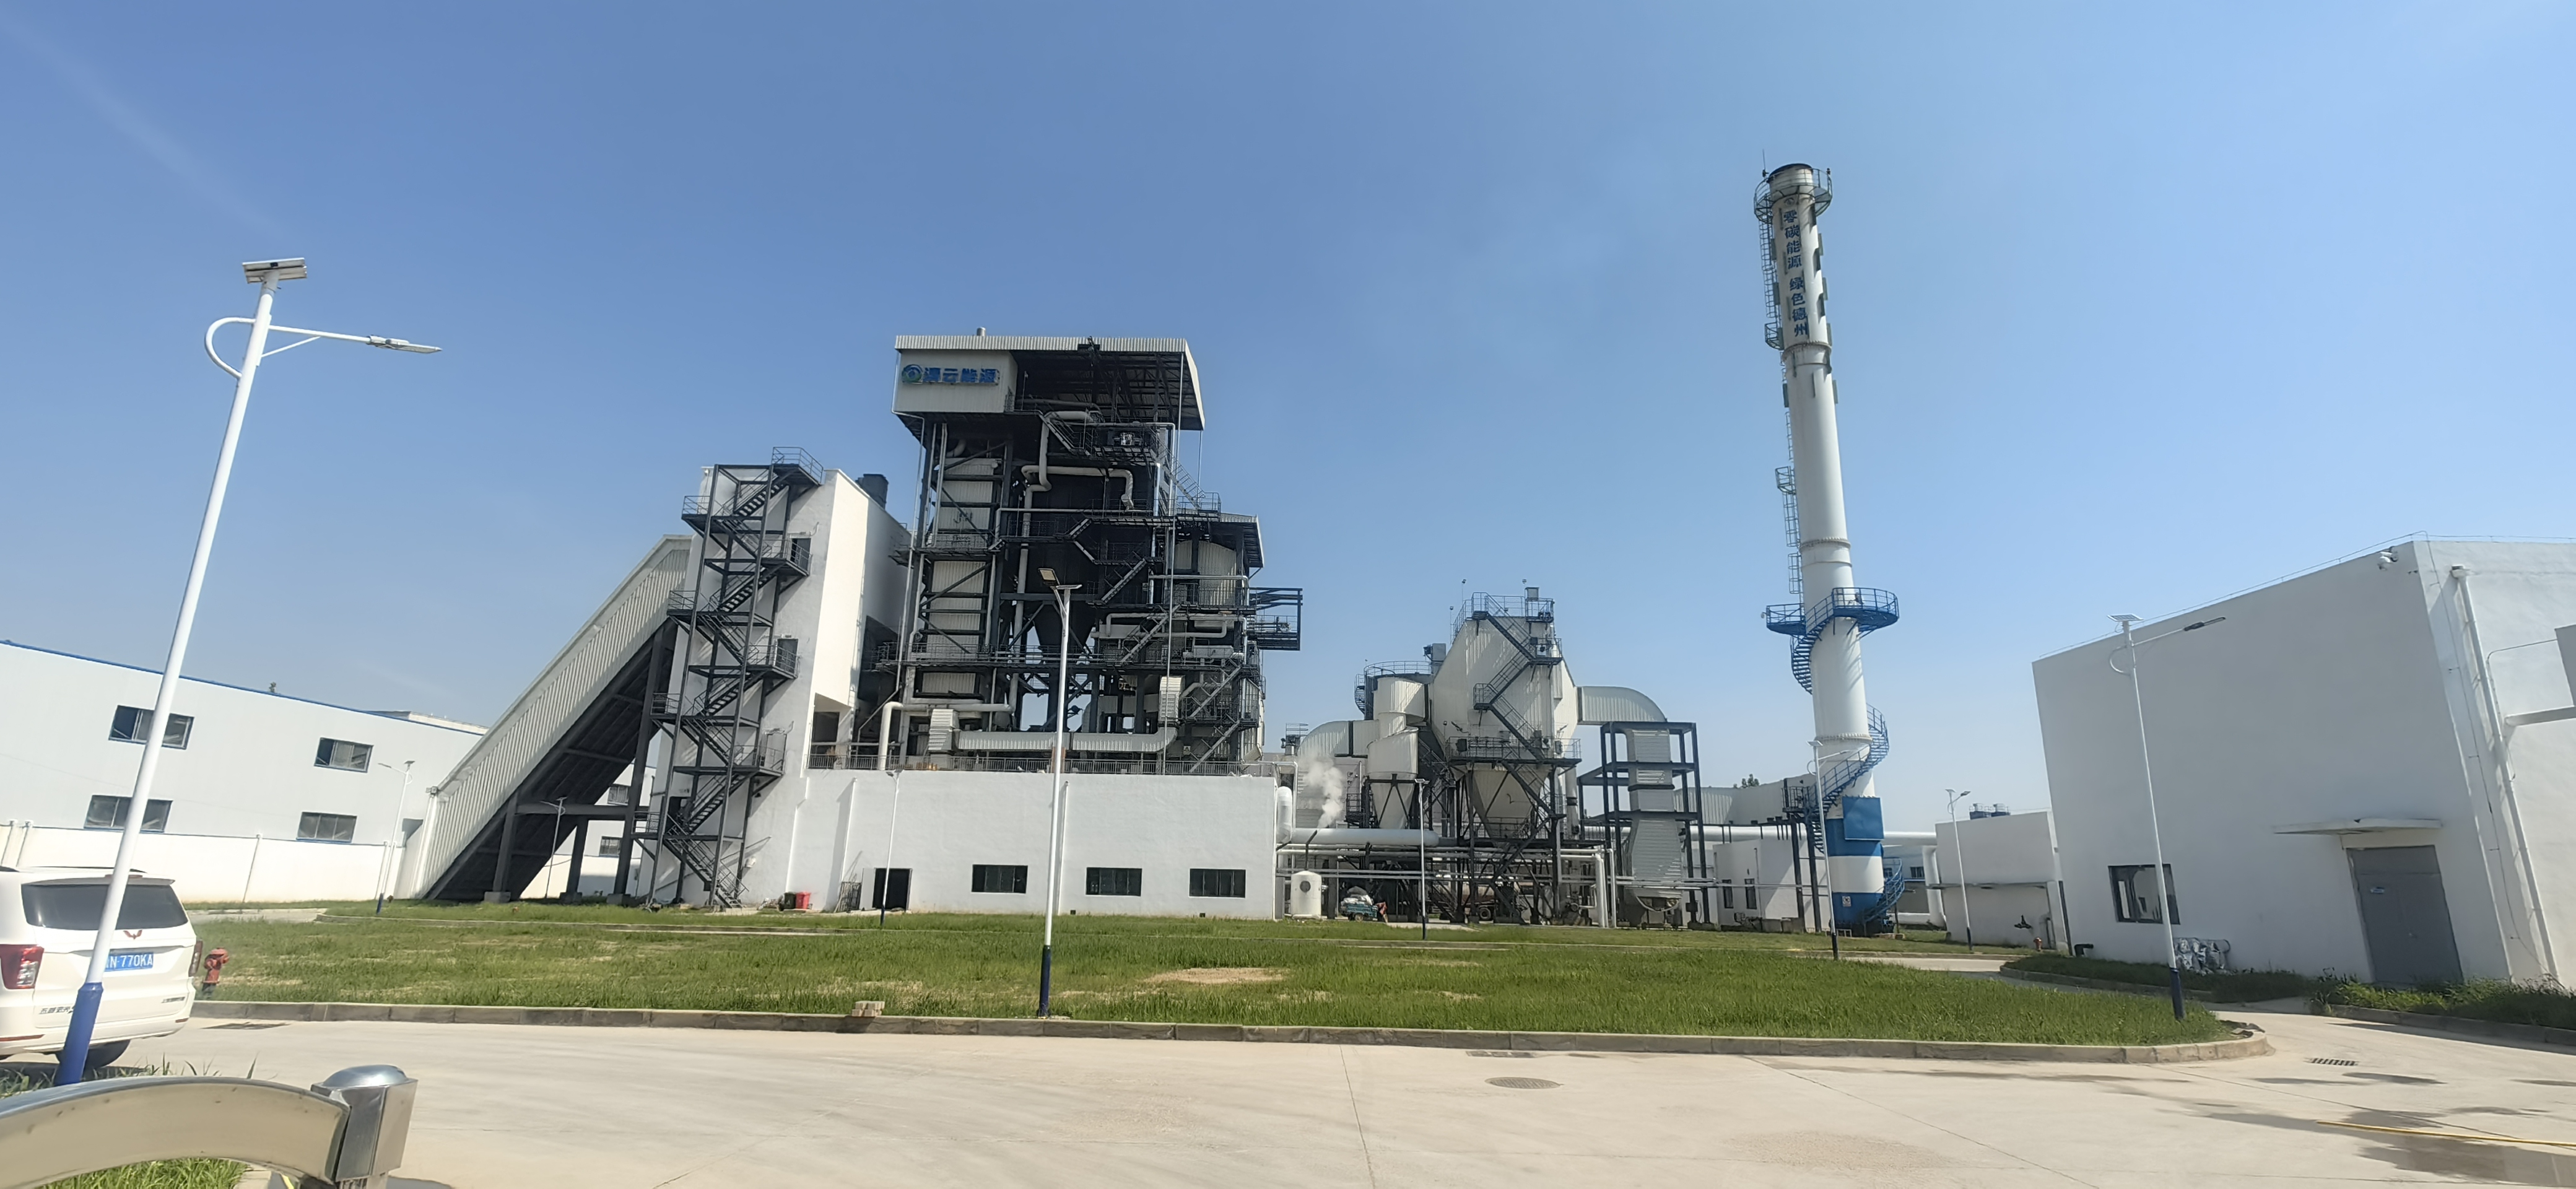
An industrial boiler manufacturer specializes in designing and producing large-scale heating systems that generate steam and hot water for industrial operations. These essential systems serve as the backbone of numerous manufacturing facilities, power plants, chemical processing centers, and district heating networks worldwide. The primary function of an industrial boiler manufacturer is to create robust boilers capable of handling extreme pressure and temperature conditions while maintaining exceptional efficiency and reliability. Modern industrial boiler manufacturer solutions incorporate advanced combustion technology, precision engineering, and sophisticated control systems that optimize fuel consumption and minimize emissions. Technologically, industrial boiler manufacturer products feature high-efficiency heat exchangers, automated fuel feeding systems, and intelligent monitoring platforms. These innovations enable operators to maximize energy output while reducing operational costs and environmental impact. Advanced materials and construction methods ensure durability in demanding industrial environments. Applications for industrial boiler manufacturer equipment span diverse sectors including textile production, food processing, pharmaceutical manufacturing, and energy generation. Heavy industries rely on these systems for continuous steam supply, process heating, and power generation. The industrial boiler manufacturer remains committed to delivering customized solutions that meet specific operational requirements and regulatory compliance standards, ensuring smooth industrial operations.

New Product Recommendations

Choosing a reputable industrial boiler manufacturer provides significant operational and financial benefits for your business. When you invest in equipment from a qualified industrial boiler manufacturer, you gain access to systems engineered for maximum efficiency and minimal downtime, directly improving your bottom line. Operational benefits are substantial and immediate. An experienced industrial boiler manufacturer designs systems that reduce fuel consumption by up to forty percent compared to older models. Your facility experiences fewer maintenance interruptions because these systems incorporate redundancy features and predictive maintenance capabilities. Operators can monitor performance in real-time through digital interfaces, catching potential issues before they become costly problems. Financially, partnering with a trusted industrial boiler manufacturer means lower energy bills and extended equipment lifespan. These systems require less frequent servicing and repairs, reducing labor costs significantly. Many industrial boiler manufacturer products qualify for tax incentives and energy rebates, providing additional savings opportunities. Environmental advantages matter increasingly to modern facilities. An industrial boiler manufacturer focuses on clean combustion technology that meets stringent emissions regulations. Your facility demonstrates environmental responsibility while maintaining production capacity. Better air quality around your facility improves worker safety and satisfaction. Application suitability varies by industry. Whether you operate a chemical plant, textile mill, or food processing facility, the right industrial boiler manufacturer customizes solutions to your specific requirements. They provide technical expertise during installation and ongoing support throughout the system's operational life. This partnership approach ensures your heating infrastructure supports growth and adapts to changing production demands effectively.

Practical Tips

What is the expected operational lifespan of a well-maintained CFB power plant?

05

Aug

What is the expected operational lifespan of a well-maintained CFB power plant?

A well-maintained cfb power plant typically operates for 30 to 40 years, with some facilities extending beyond 40 years through rigorous maintenance and technological upgrades. The operational lifespan depends heavily on design quality, maintenance p...
View More
How to troubleshoot oxygen distribution issues in an industrial CFB boiler?

08

Sep

How to troubleshoot oxygen distribution issues in an industrial CFB boiler?

Oxygen distribution challenges represent one of the most critical operational issues affecting industrial boiler performance and energy efficiency. In a cfb boiler, proper air supply regulation directly impacts combustion quality, fuel consumption ra...
View More
What temperature range ensures optimal efficiency in fluidized bed combustion?

25

Sep

What temperature range ensures optimal efficiency in fluidized bed combustion?

Understanding the optimal temperature range for fluidized bed combustion is essential for operators seeking to maximize boiler performance and reduce operational costs. Temperature control directly influences combustion efficiency, fuel consumption r...
View More
How does a circulating fluidized bed optimize the combustion residence time?

22

Oct

How does a circulating fluidized bed optimize the combustion residence time?

The circulating fluidized bed represents a transformative approach to combustion optimization in industrial power generation. Unlike traditional fixed-bed systems, this technology maintains fuel particles in continuous suspension within the combustio...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial boiler manufacturer

Advanced Efficiency Technology

Advanced Efficiency Technology

Leading industrial boiler manufacturer systems incorporate state-of-the-art heat recovery mechanisms that capture waste heat from exhaust gases. This technology transforms potential energy loss into productive output, significantly reducing overall fuel requirements. An industrial boiler manufacturer utilizing these innovations helps facilities achieve efficiency ratings exceeding ninety percent, substantially lower than conventional equipment. The advanced combustion controls automatically adjust fuel-air mixtures based on real-time demand, preventing wasteful overheating and optimizing performance across varying operational loads. Modern industrial boiler manufacturer solutions feature modulating burners that respond dynamically to facility demands, ensuring consistent performance whether operating at partial load or full capacity. These efficiency improvements directly translate to reduced operating expenses and faster return on investment for facilities upgrading their thermal infrastructure.
Reliable Performance and Durability

Reliable Performance and Durability

An experienced industrial boiler manufacturer builds systems designed to withstand decades of continuous operation in challenging environments. Premium materials and rigorous quality control standards ensure every unit from a reputable industrial boiler manufacturer meets demanding international specifications. The construction methodology incorporates reinforced components that resist thermal stress, corrosion, and mechanical wear from sustained high-pressure operation. When you select an industrial boiler manufacturer with proven experience, you gain equipment featuring redundant safety systems and fail-safe mechanisms protecting your investment and facility personnel. Extended warranties backed by industrial boiler manufacturer service networks provide peace of mind and financial protection. These durable systems minimize unexpected breakdowns that disrupt production schedules, maintaining operational continuity and protecting revenue streams for manufacturing facilities.
Comprehensive Technical Support and Customization

Comprehensive Technical Support and Customization

A professional industrial boiler manufacturer doesn't simply deliver equipment; they provide complete lifecycle support from initial consultation through decommissioning. Expert teams from any industrial boiler manufacturer evaluate your facility's unique requirements, designing tailored solutions matching specific capacity, fuel type, and operational parameters. Installation services from qualified industrial boiler manufacturer technicians ensure proper setup and system optimization. Ongoing training programs equip your operators with knowledge to maximize equipment performance and identify maintenance needs early. Responsive industrial boiler manufacturer support teams assist with troubleshooting, spare parts procurement, and performance optimization. Many industrial boiler manufacturer providers offer remote monitoring services that track system health continuously, scheduling preventive maintenance before problems develop and ensuring your heating infrastructure operates reliably year-round.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
email goToTop