Coal Boiler Manufacturers

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

coal boiler manufacturers

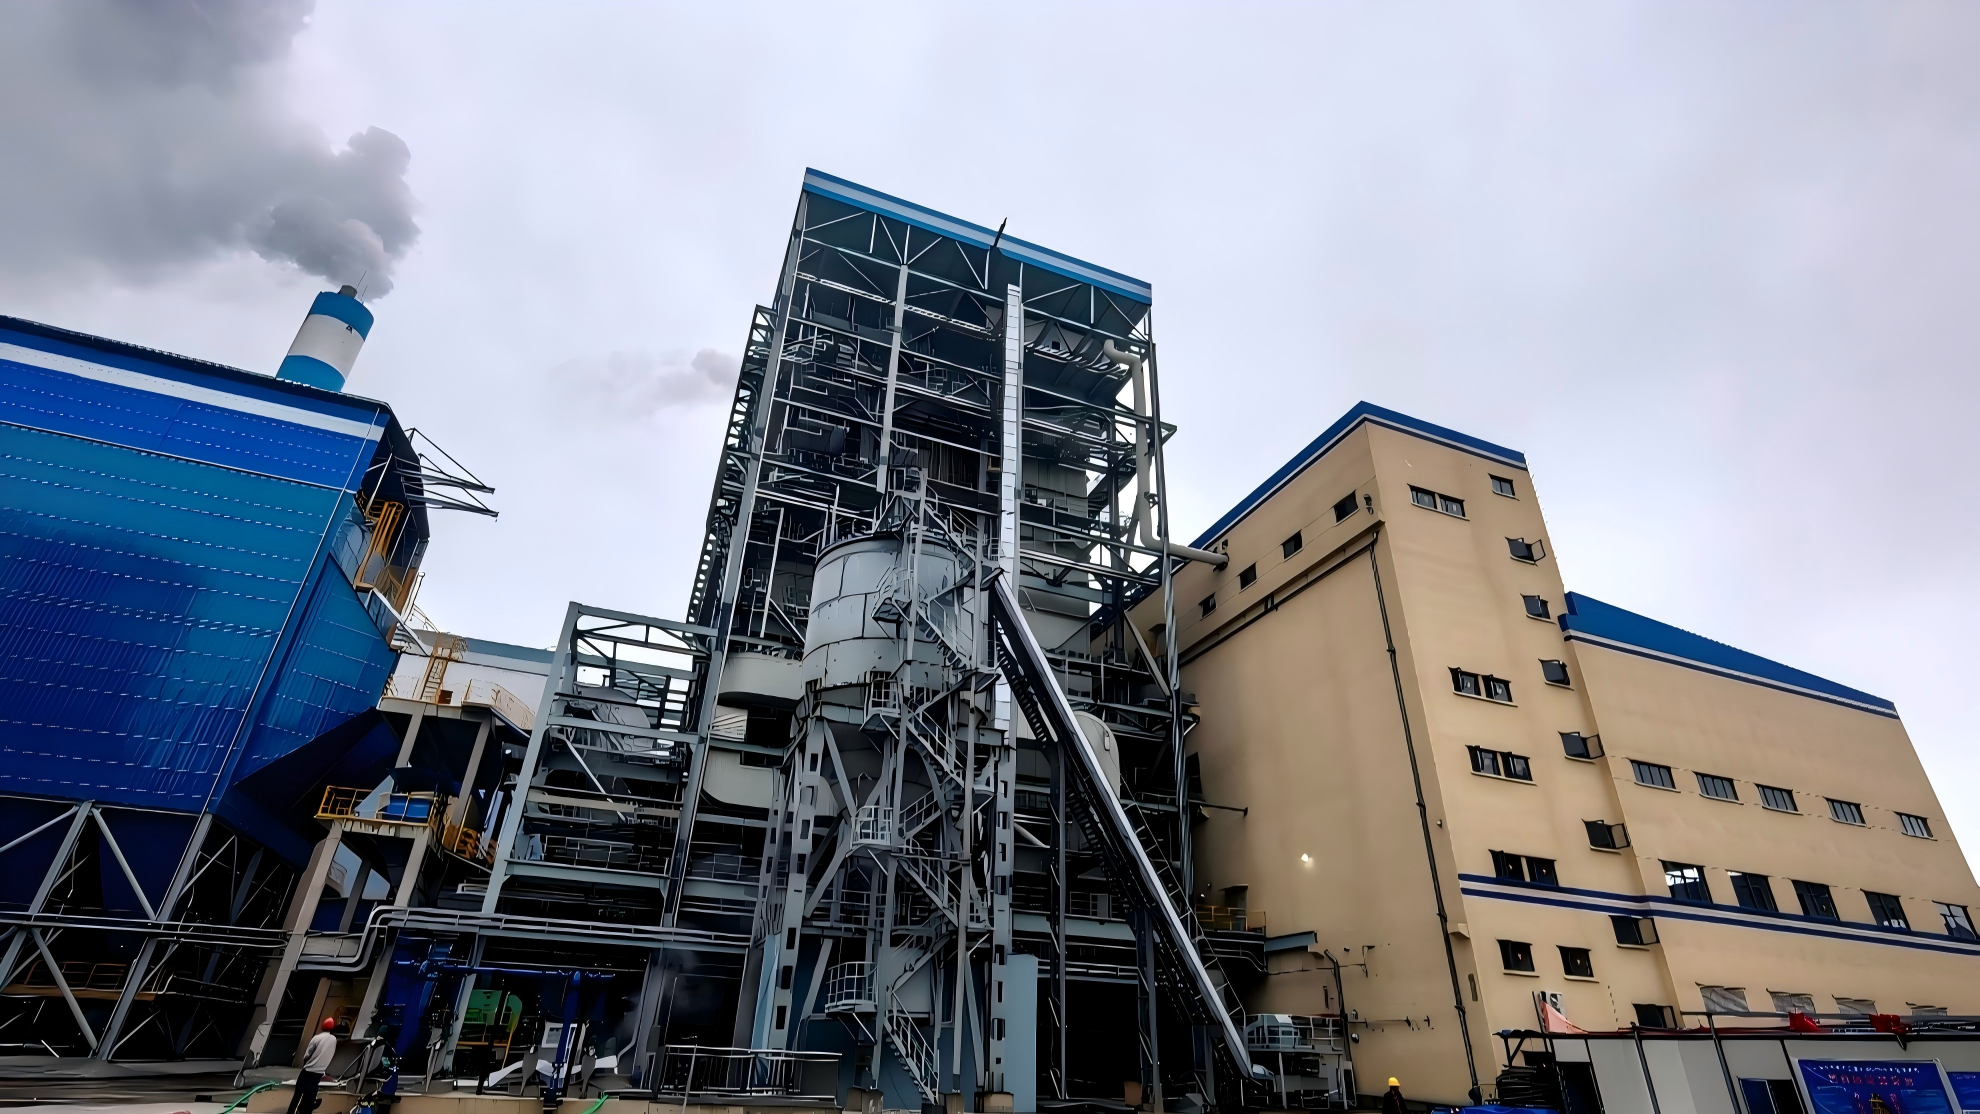
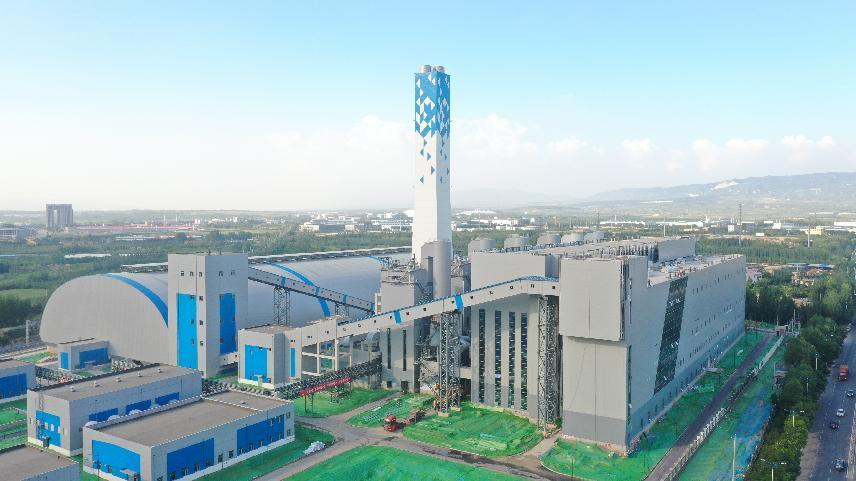
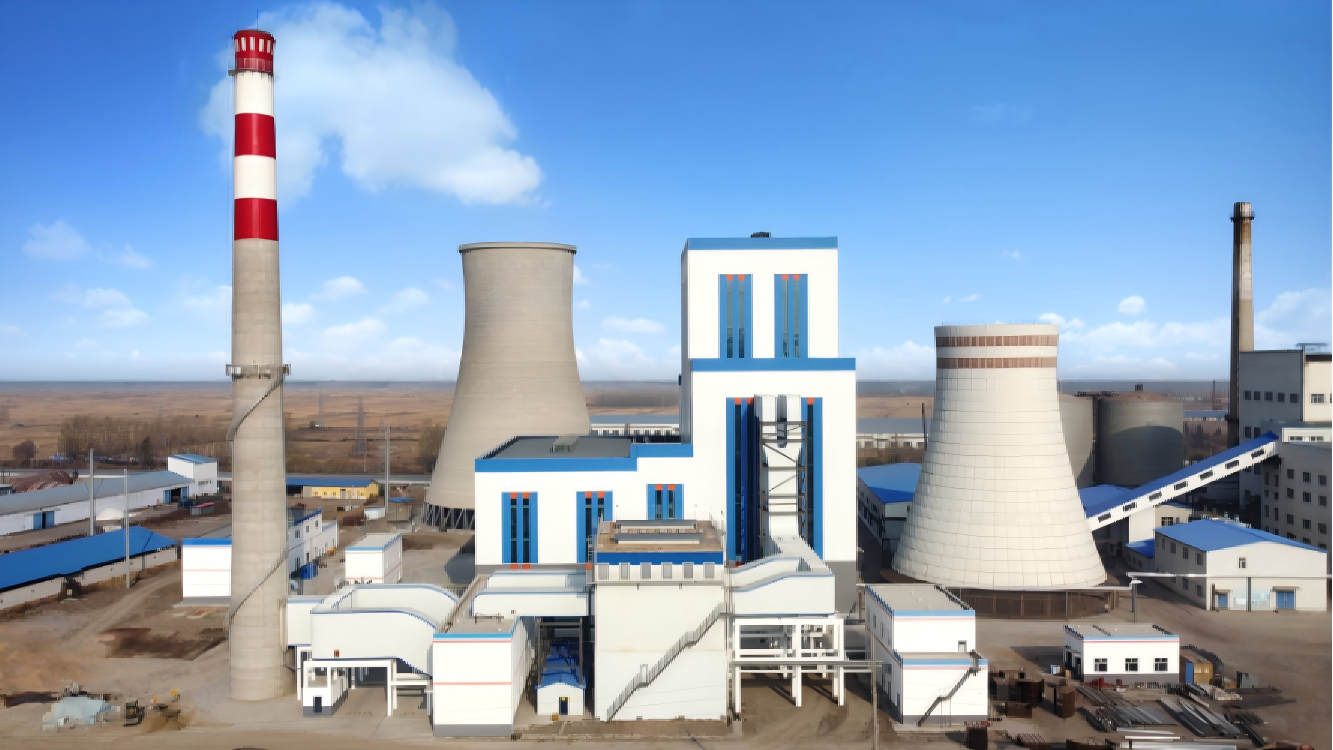
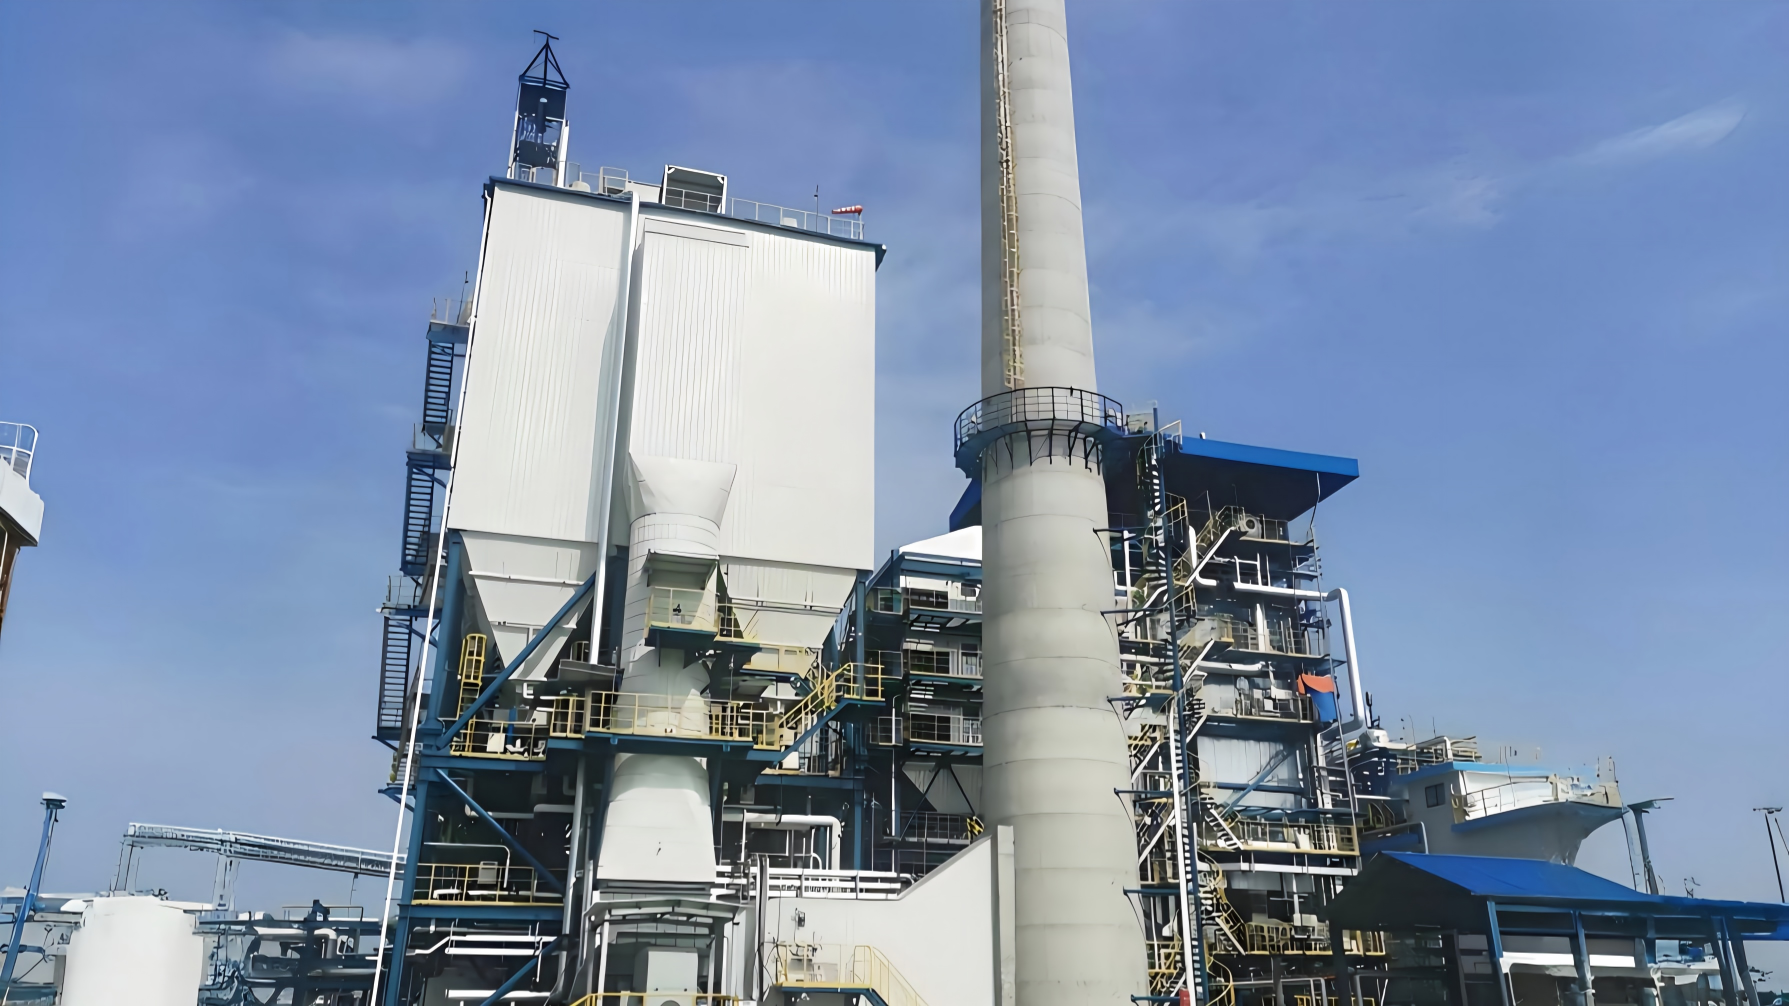
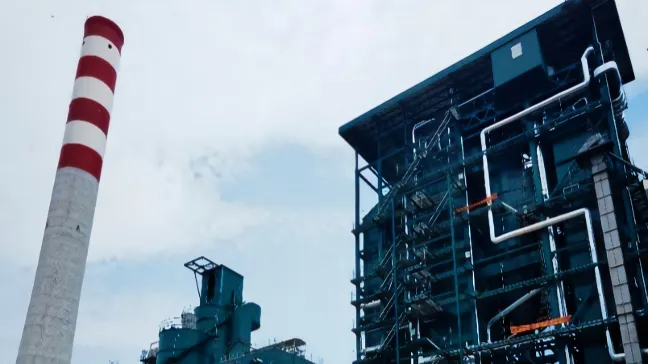
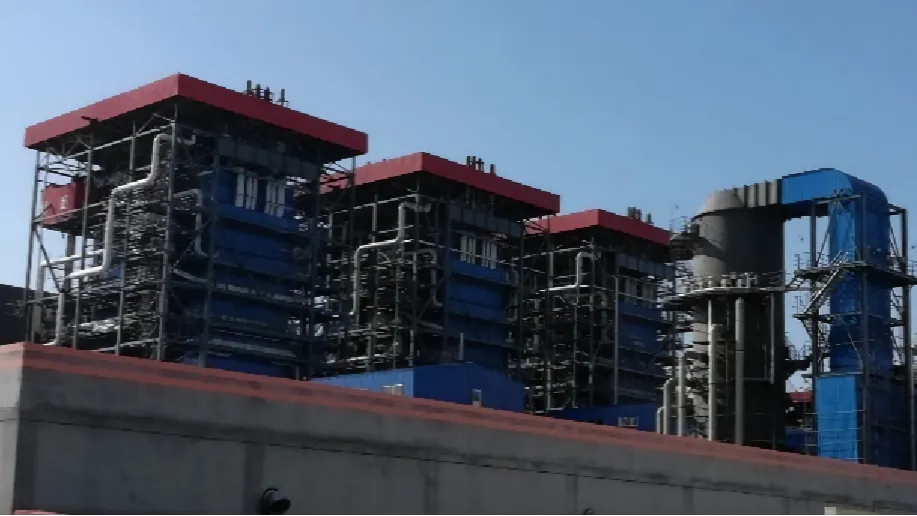
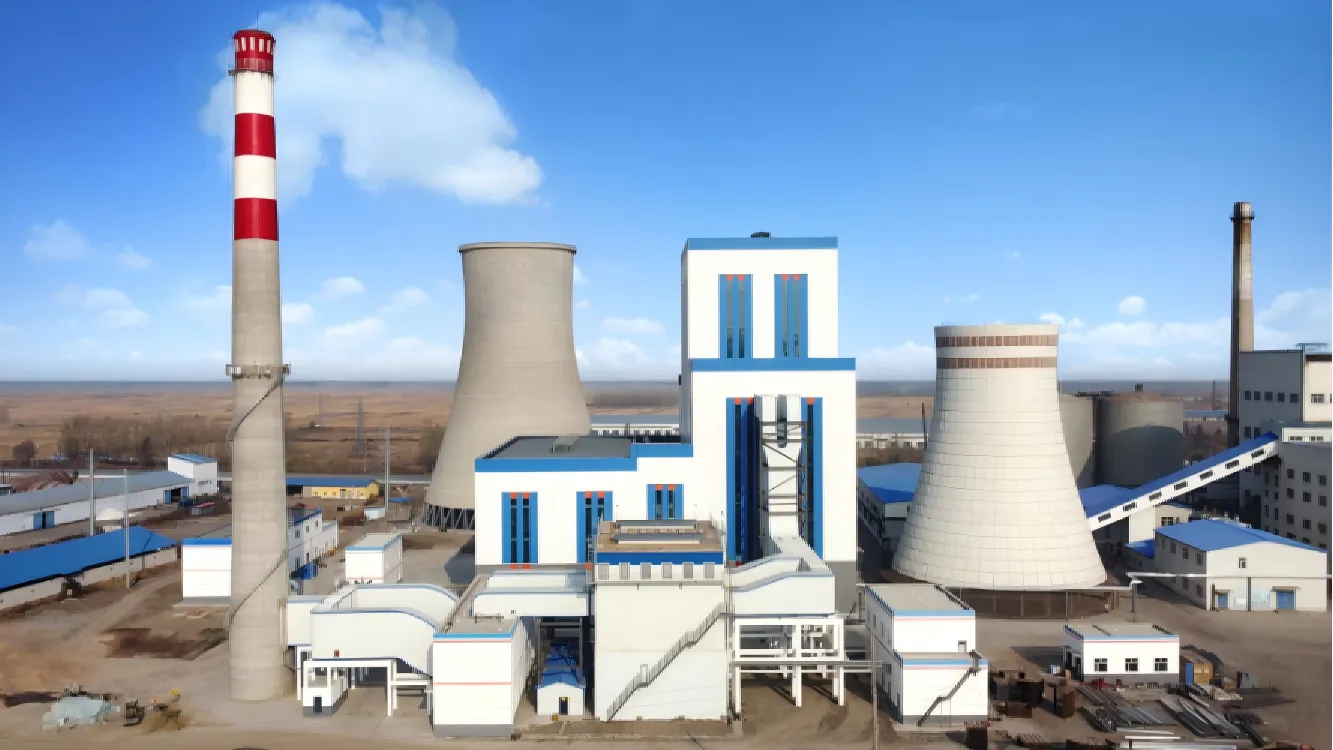
Coal boiler manufacturers produce essential industrial heating equipment designed to convert coal fuel into thermal energy for various commercial and residential applications. These specialists in boiler production create systems that efficiently burn coal to generate steam or hot water, which then powers machinery, heating systems, and electricity generation across multiple industries. The main functions of coal boiler manufacturers involve designing and constructing robust boilers capable of withstanding high temperatures and pressures while maintaining optimal combustion efficiency. Coal boiler manufacturers focus on producing units that safely handle coal fuel types, including bituminous coal, anthracite, and lignite, adapting their designs to accommodate different coal qualities and moisture content. Technological features of modern coal boiler manufacturers include advanced combustion control systems, automated fuel feeding mechanisms, and sophisticated emission reduction technology. These innovations help coal boiler manufacturers create equipment that meets stringent environmental regulations while maximizing energy output. Modern units incorporate specialized grates, ash handling systems, and water circulation designs that improve performance and reduce maintenance requirements. Applications of products from coal boiler manufacturers span diverse sectors including power generation plants, industrial manufacturing facilities, district heating systems, and institutional buildings. Coal boiler manufacturers serve chemical plants, paper mills, and textile factories where reliable heat generation remains critical for operations. Their equipment also supports heating infrastructure in regions where coal remains a primary energy source, providing consistent and dependable thermal energy solutions for communities and businesses seeking durable heating systems.

New Product Releases

Selecting equipment from reputable coal boiler manufacturers provides significant operational and financial benefits for your business needs. These manufacturers deliver solutions that offer superior reliability and extended service life, reducing costly downtime and replacement expenses. By choosing established coal boiler manufacturers, you gain access to systems engineered for maximum fuel efficiency, which directly lowers your operational energy costs and improves your bottom line. Coal boiler manufacturers design their equipment to accommodate various coal types and qualities, providing flexibility for facilities operating in diverse geographic regions or sourcing fuel from multiple suppliers. This adaptability ensures your heating system performs consistently regardless of fuel variations, protecting your investment against supply chain disruptions. The robust construction standards maintained by coal boiler manufacturers mean your equipment withstands demanding industrial conditions, harsh environments, and continuous operation without premature failure. Modern coal boiler manufacturers incorporate advanced emission control technologies that help your facility comply with environmental regulations and reduce your carbon footprint. These manufacturers engineer systems with automated controls and safety features that protect your personnel and equipment, minimizing accident risks and liability concerns. Additionally, coal boiler manufacturers provide comprehensive technical support, spare parts availability, and maintenance guidance that extends equipment lifespan and ensures optimal performance throughout its operational life. For facilities seeking cost-effective large-scale heating solutions, coal boiler manufacturers offer unmatched value through scalable systems designed for institutional, industrial, and commercial applications. The established expertise of coal boiler manufacturers in system design, installation support, and performance optimization ensures your heating infrastructure meets current demands while accommodating future expansion requirements. Their commitment to quality manufacturing and customer service builds long-term partnerships that support your operational success and profitability.

Latest News

What is the expected operational lifespan of a well-maintained CFB power plant?

05

Aug

What is the expected operational lifespan of a well-maintained CFB power plant?

A well-maintained cfb power plant typically operates for 30 to 40 years, with some facilities extending beyond 40 years through rigorous maintenance and technological upgrades. The operational lifespan depends heavily on design quality, maintenance p...
View More
How to troubleshoot oxygen distribution issues in an industrial CFB boiler?

08

Sep

How to troubleshoot oxygen distribution issues in an industrial CFB boiler?

Oxygen distribution challenges represent one of the most critical operational issues affecting industrial boiler performance and energy efficiency. In a cfb boiler, proper air supply regulation directly impacts combustion quality, fuel consumption ra...
View More
How does fluidized bed combustion adapt to sudden fuel composition shifts?

15

Sep

How does fluidized bed combustion adapt to sudden fuel composition shifts?

Fuel composition variability remains one of the most challenging operational parameters in modern thermal power generation. When feedstock sources shift unexpectedly or intentionally blend different materials, systems must respond quickly to maintain...
View More
What are the mechanical components prone to wear in fluidized bed combustion?

22

Sep

What are the mechanical components prone to wear in fluidized bed combustion?

Fluidized bed combustion remains one of the most efficient and environmentally sound fuel-burning methods in industrial power generation. However, understanding the mechanical components prone to wear in fluidized bed combustion is essential for oper...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

coal boiler manufacturers

Advanced Combustion Technology for Maximum Efficiency

Advanced Combustion Technology for Maximum Efficiency

Coal boiler manufacturers integrate cutting-edge combustion control systems that optimize fuel burning and heat transfer, delivering superior thermal efficiency compared to conventional heating solutions. These advanced systems utilize precision air-fuel ratio management, automated staging controls, and real-time monitoring technology to ensure complete coal combustion while minimizing waste. Coal boiler manufacturers engineer their equipment with enhanced furnace designs and specialized flame management features that extract maximum heat energy from every unit of fuel consumed. The result is measurably reduced fuel consumption and lower operational costs for your facility. Modern coal boiler manufacturers prioritize efficiency improvements that significantly decrease your energy expenses over the equipment's lifetime, making these investments highly cost-effective. Their combustion technology also reduces unburned carbon in ash residue, improving overall system performance and minimizing environmental impact while maximizing your return on investment.
Comprehensive Emission Control and Environmental Compliance

Comprehensive Emission Control and Environmental Compliance

Leading coal boiler manufacturers equip their systems with sophisticated emission reduction technologies that ensure compliance with strict environmental regulations worldwide. These manufacturers integrate advanced dust collectors, flue gas treatment systems, and pollution control equipment that significantly reduce particulate matter, sulfur dioxide, and nitrogen oxide emissions. Coal boiler manufacturers design their environmental systems to maintain excellent air quality around your facility while protecting your operational licenses and avoiding expensive regulatory penalties. Their commitment to sustainable manufacturing reflects industry best practices and demonstrates responsibility toward environmental stewardship. Coal boiler manufacturers continuously update their technology to meet evolving emission standards, protecting your long-term regulatory compliance and reducing future retrofitting costs. By selecting equipment from environmentally conscious coal boiler manufacturers, you align your operations with contemporary environmental values while ensuring your heating infrastructure remains compliant with future regulatory changes and demonstrates corporate environmental commitment.
Dependable Service Support and Spare Parts Availability

Dependable Service Support and Spare Parts Availability

Reputable coal boiler manufacturers provide comprehensive after-sale support services including technical assistance, preventive maintenance programs, and rapid spare parts availability that minimize equipment downtime and maximize operational continuity. Coal boiler manufacturers maintain extensive spare parts inventory and strategic distribution networks ensuring replacement components reach your facility quickly when needed. Their experienced technical teams offer training, troubleshooting guidance, and performance optimization consulting that extends equipment lifespan and improves efficiency. Coal boiler manufacturers establish long-term service partnerships that provide peace of mind knowing expert support remains accessible throughout your equipment's operational life. With dedicated customer service representatives and responsive technical hotlines, coal boiler manufacturers ensure your facility receives priority attention during critical situations. This commitment to comprehensive support distinguishes quality manufacturers and protects your operational investment, preventing costly extended shutdowns and maintaining your facility's heating reliability for consistent business operations.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
email goToTop