Industrial CFB Boiler Manufacturer Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial cfb boiler manufacturer

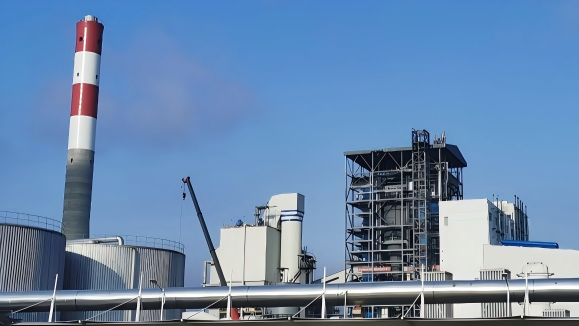
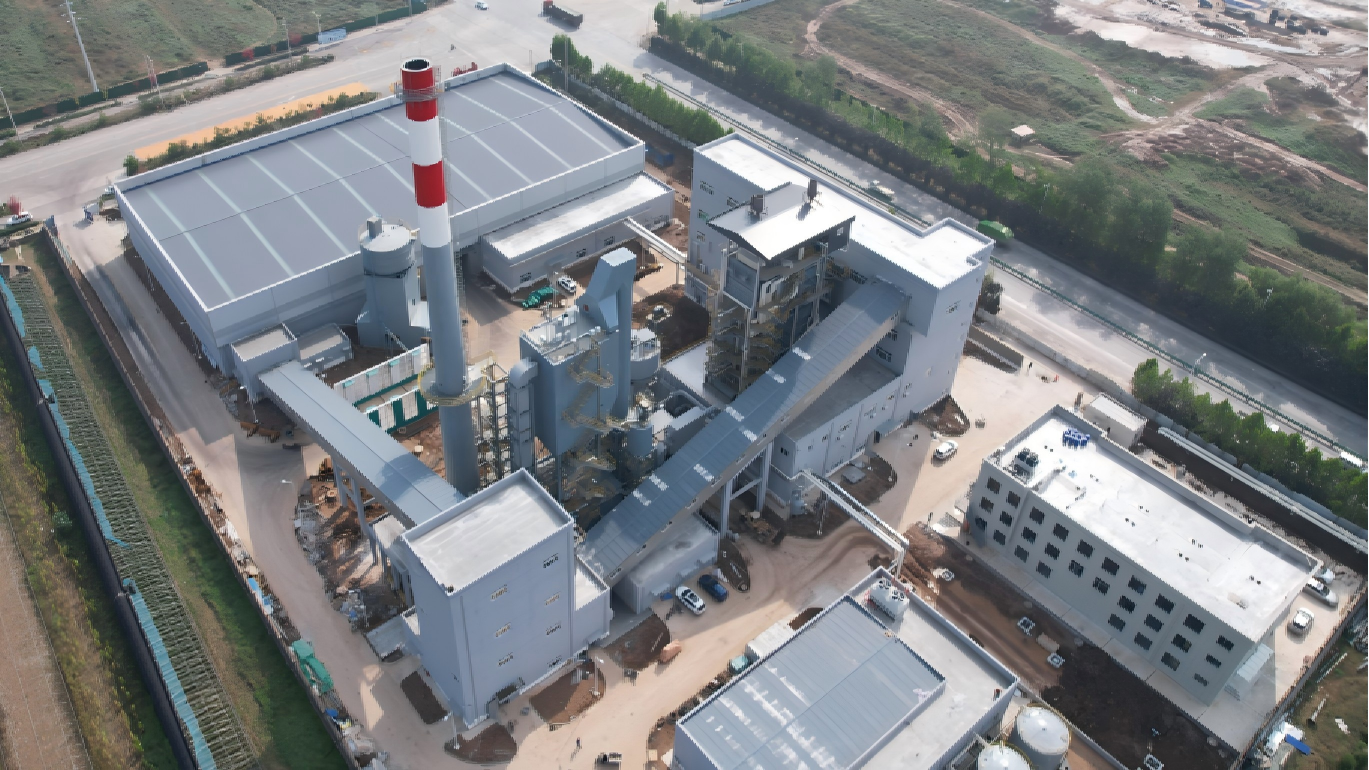
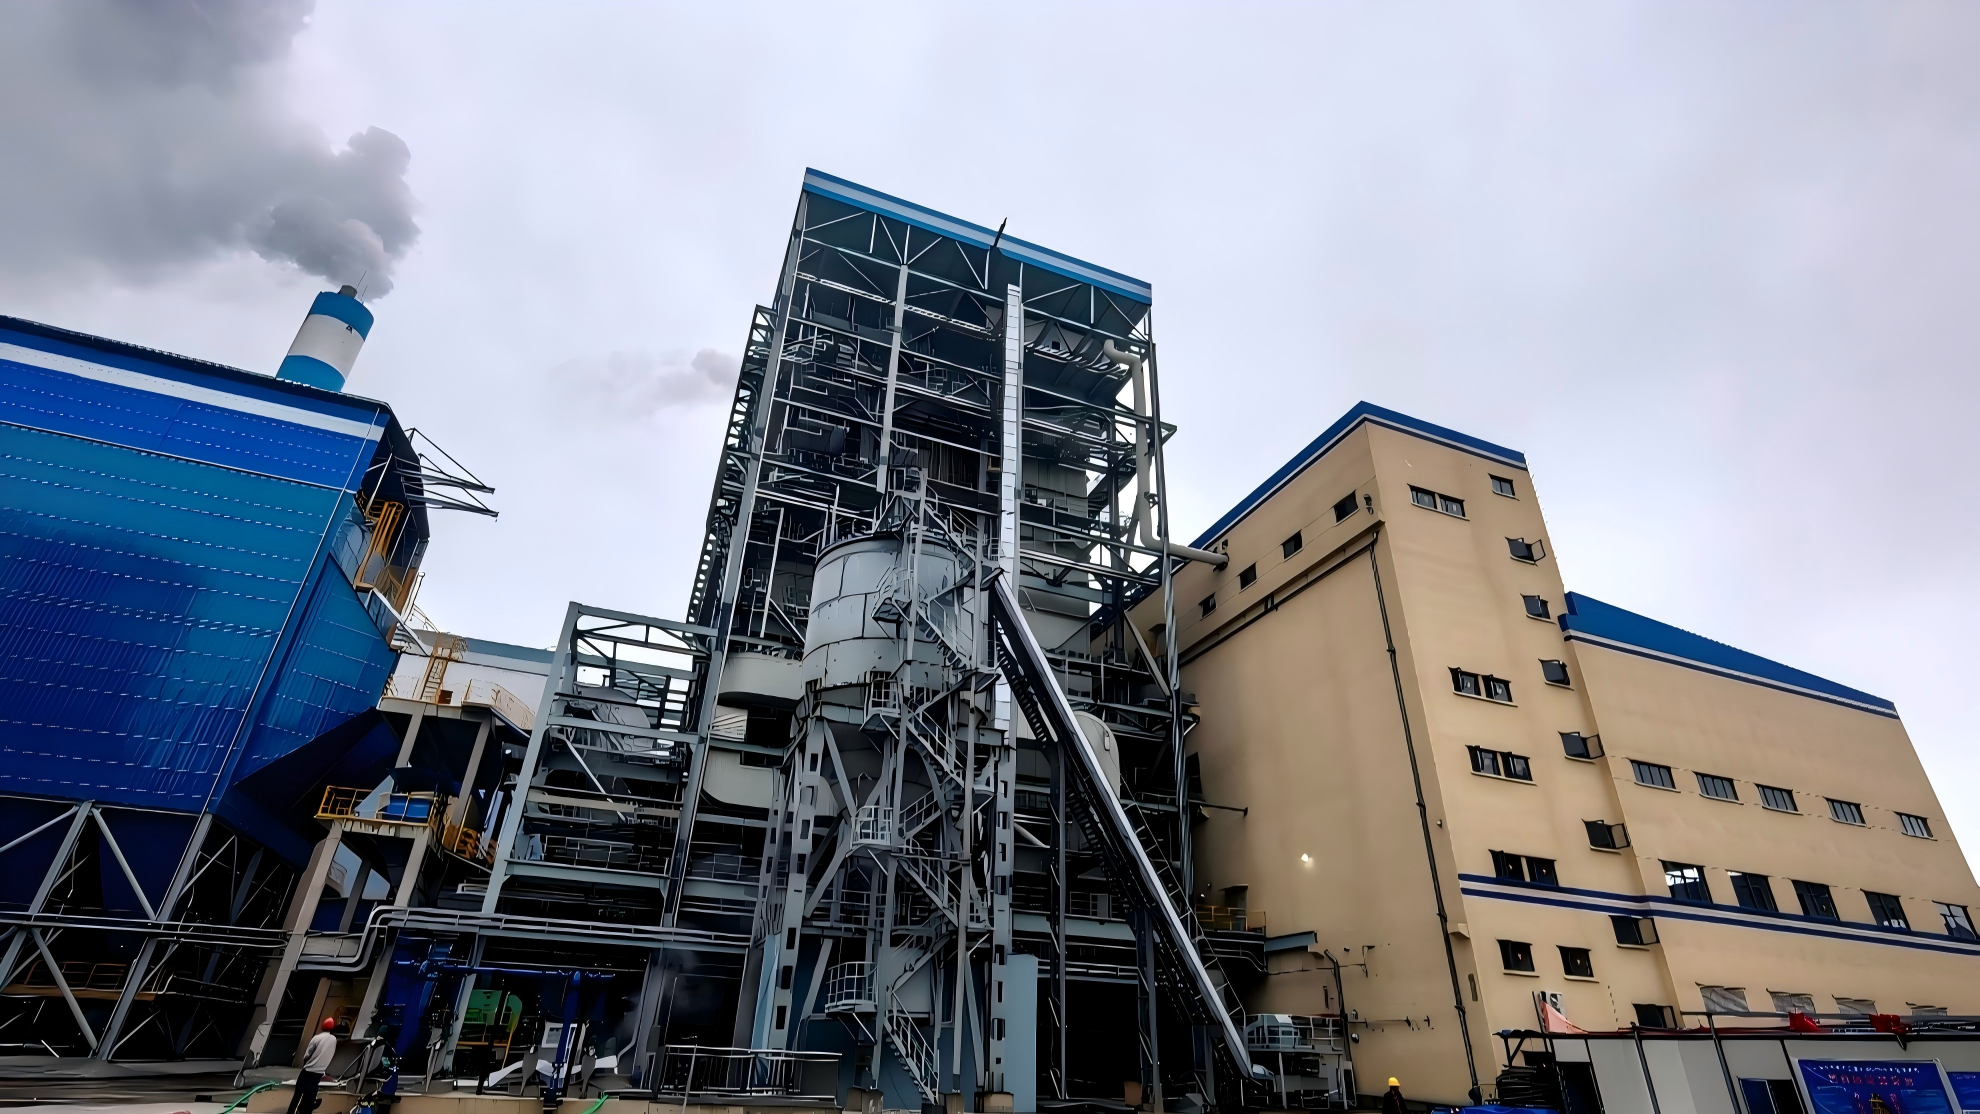
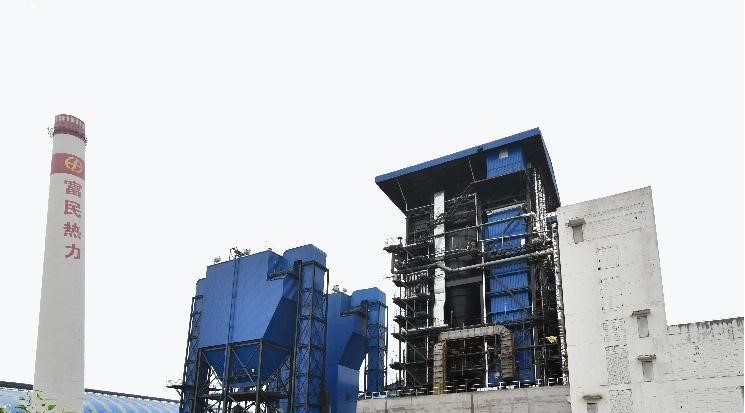
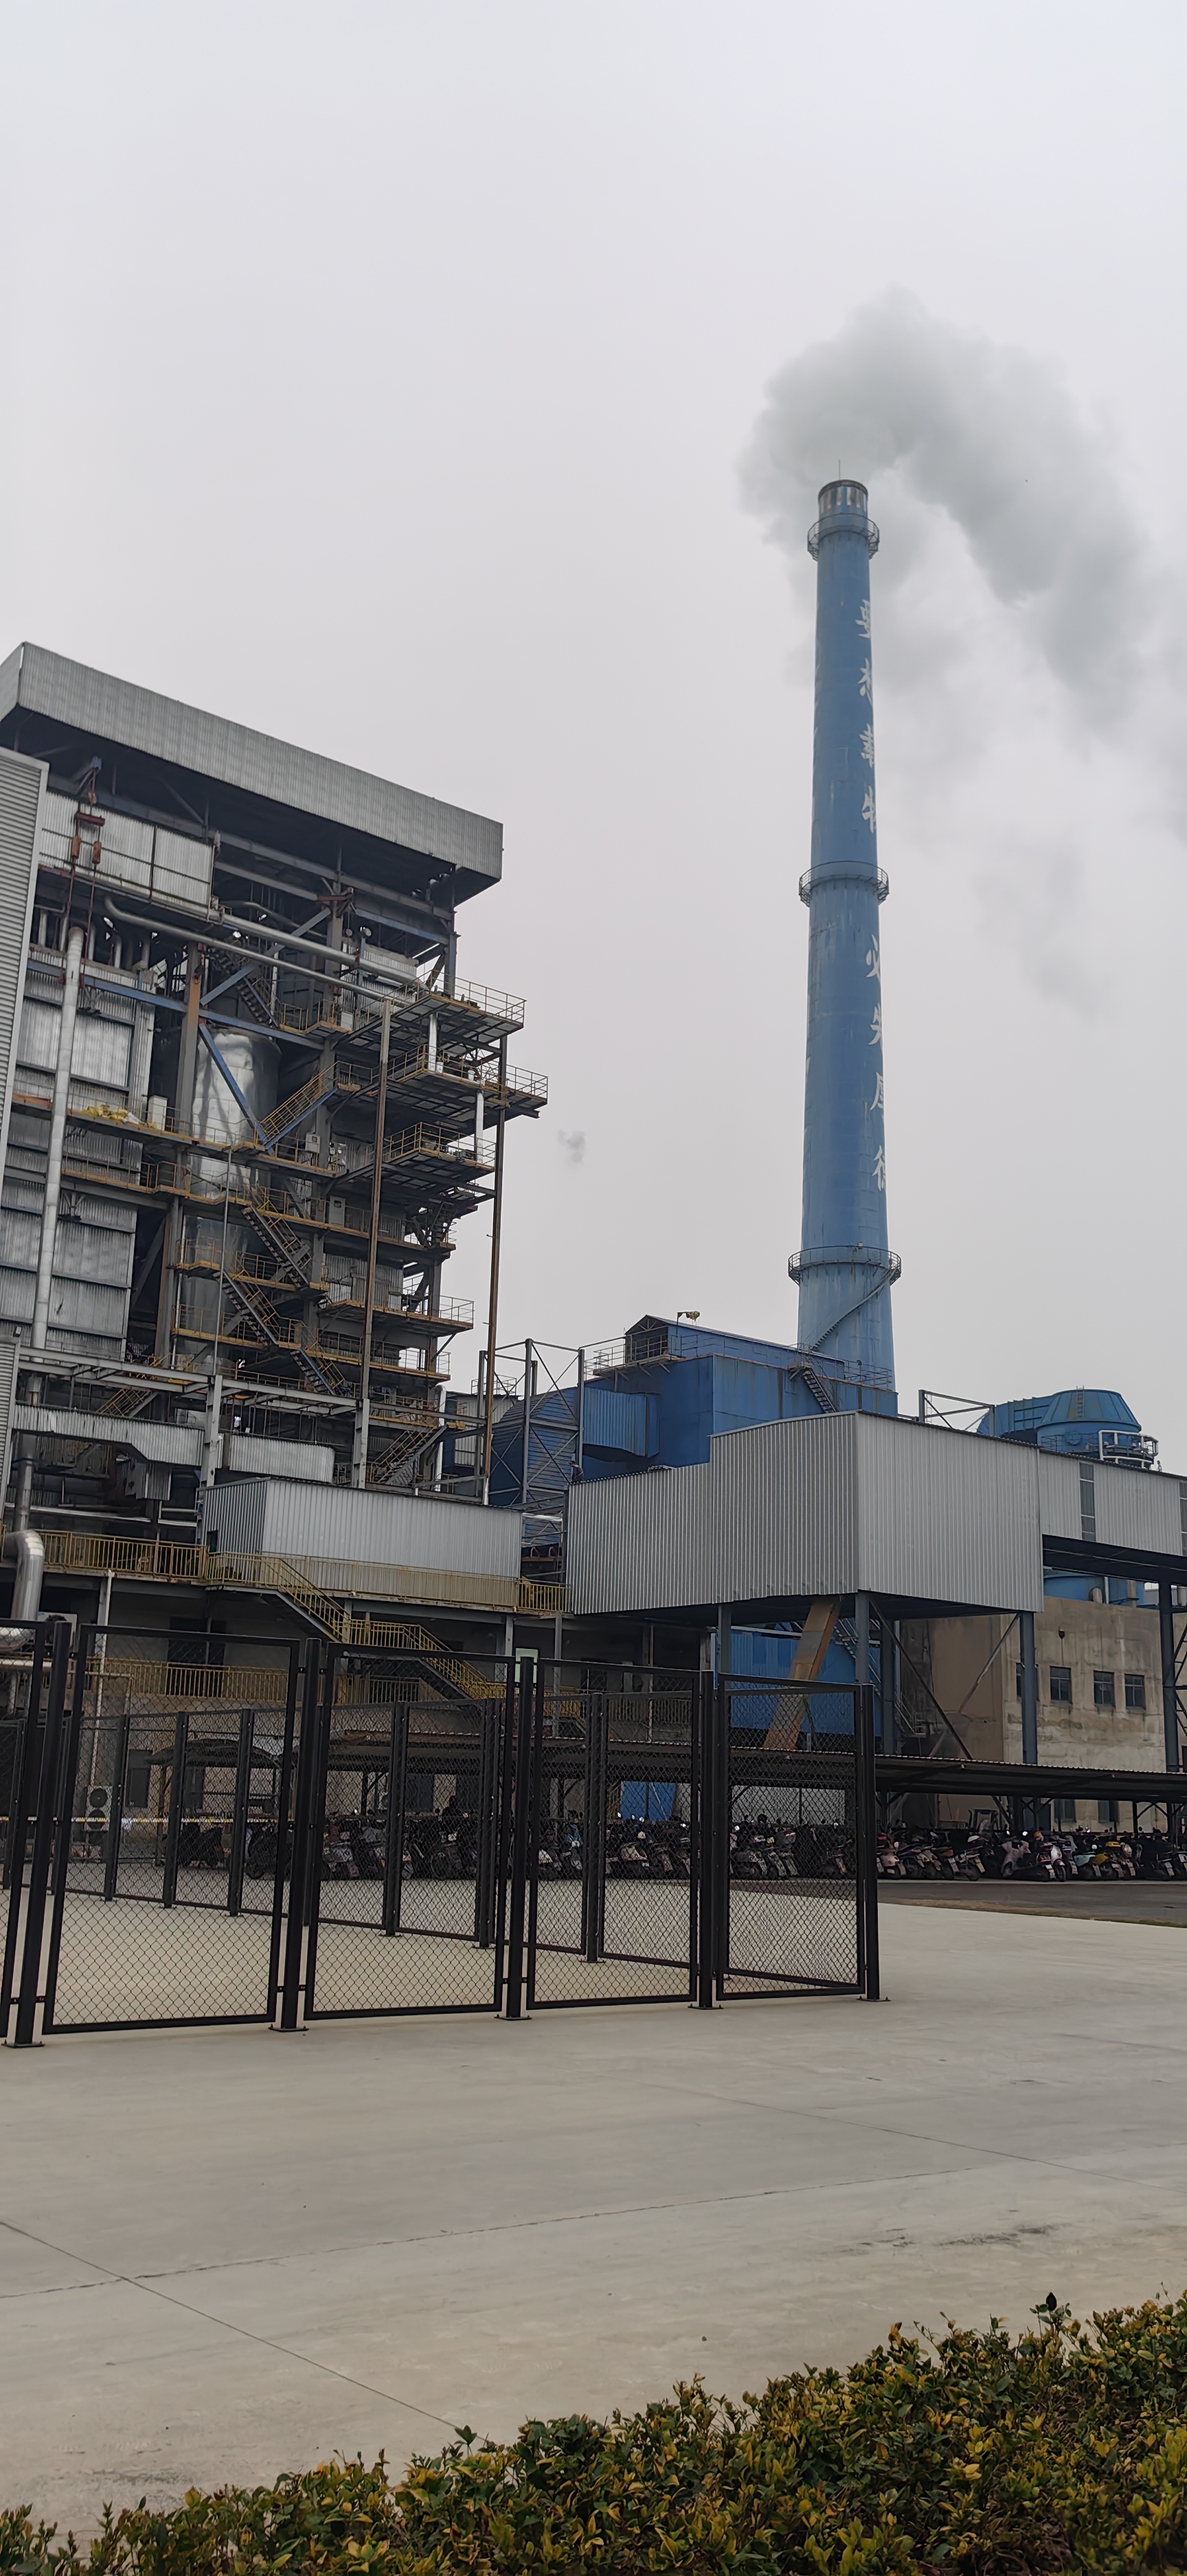
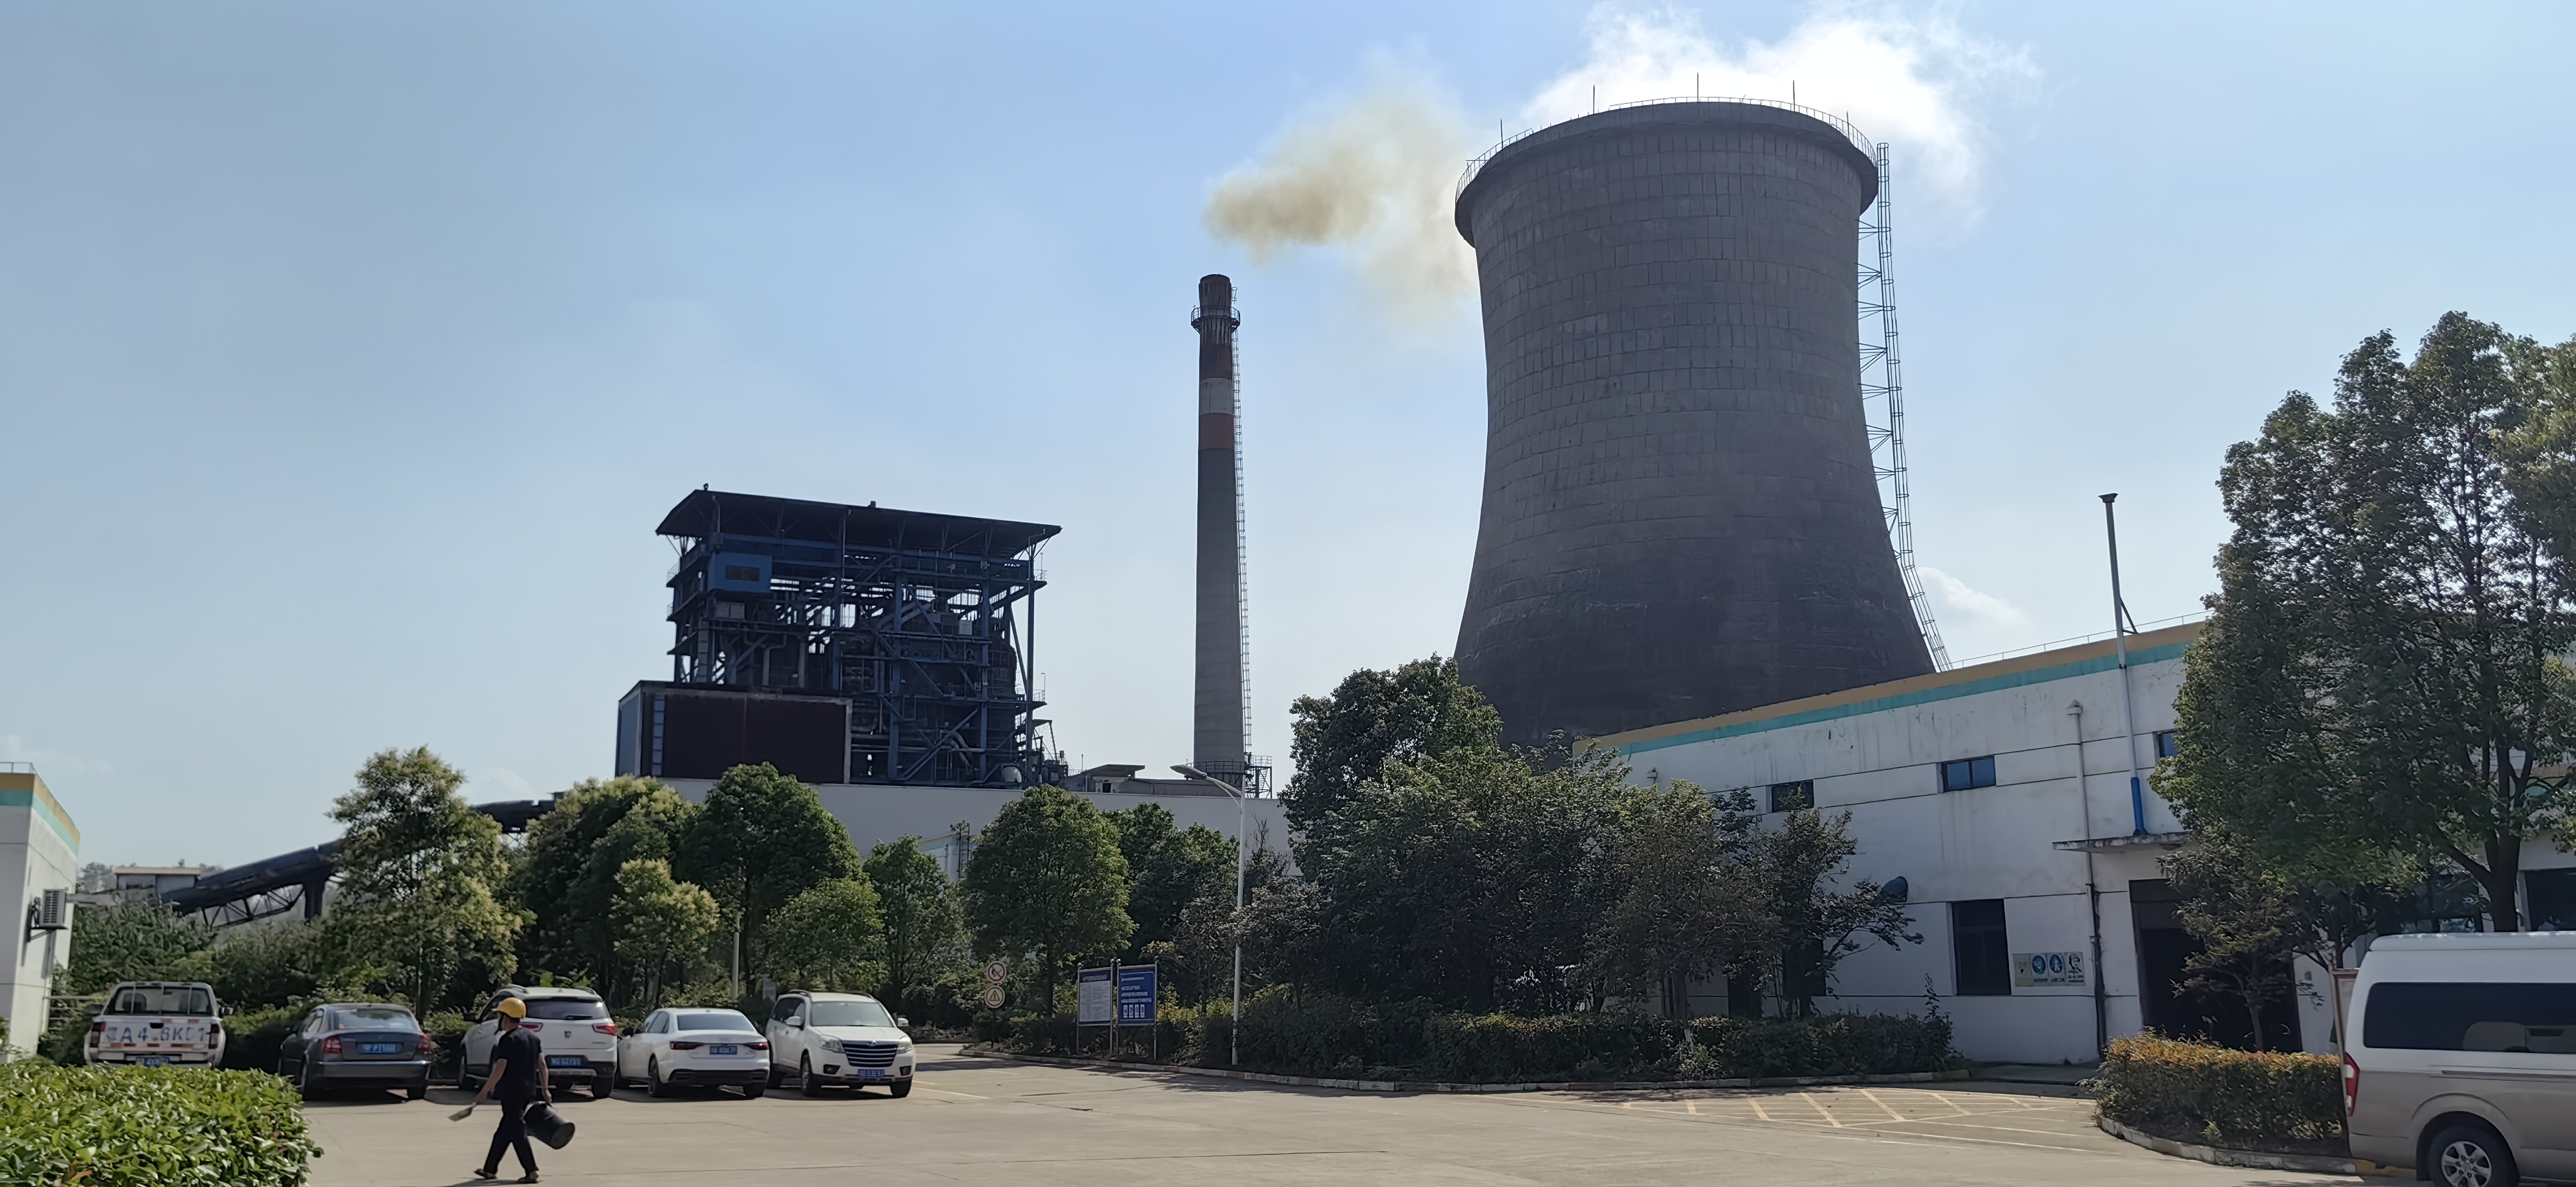
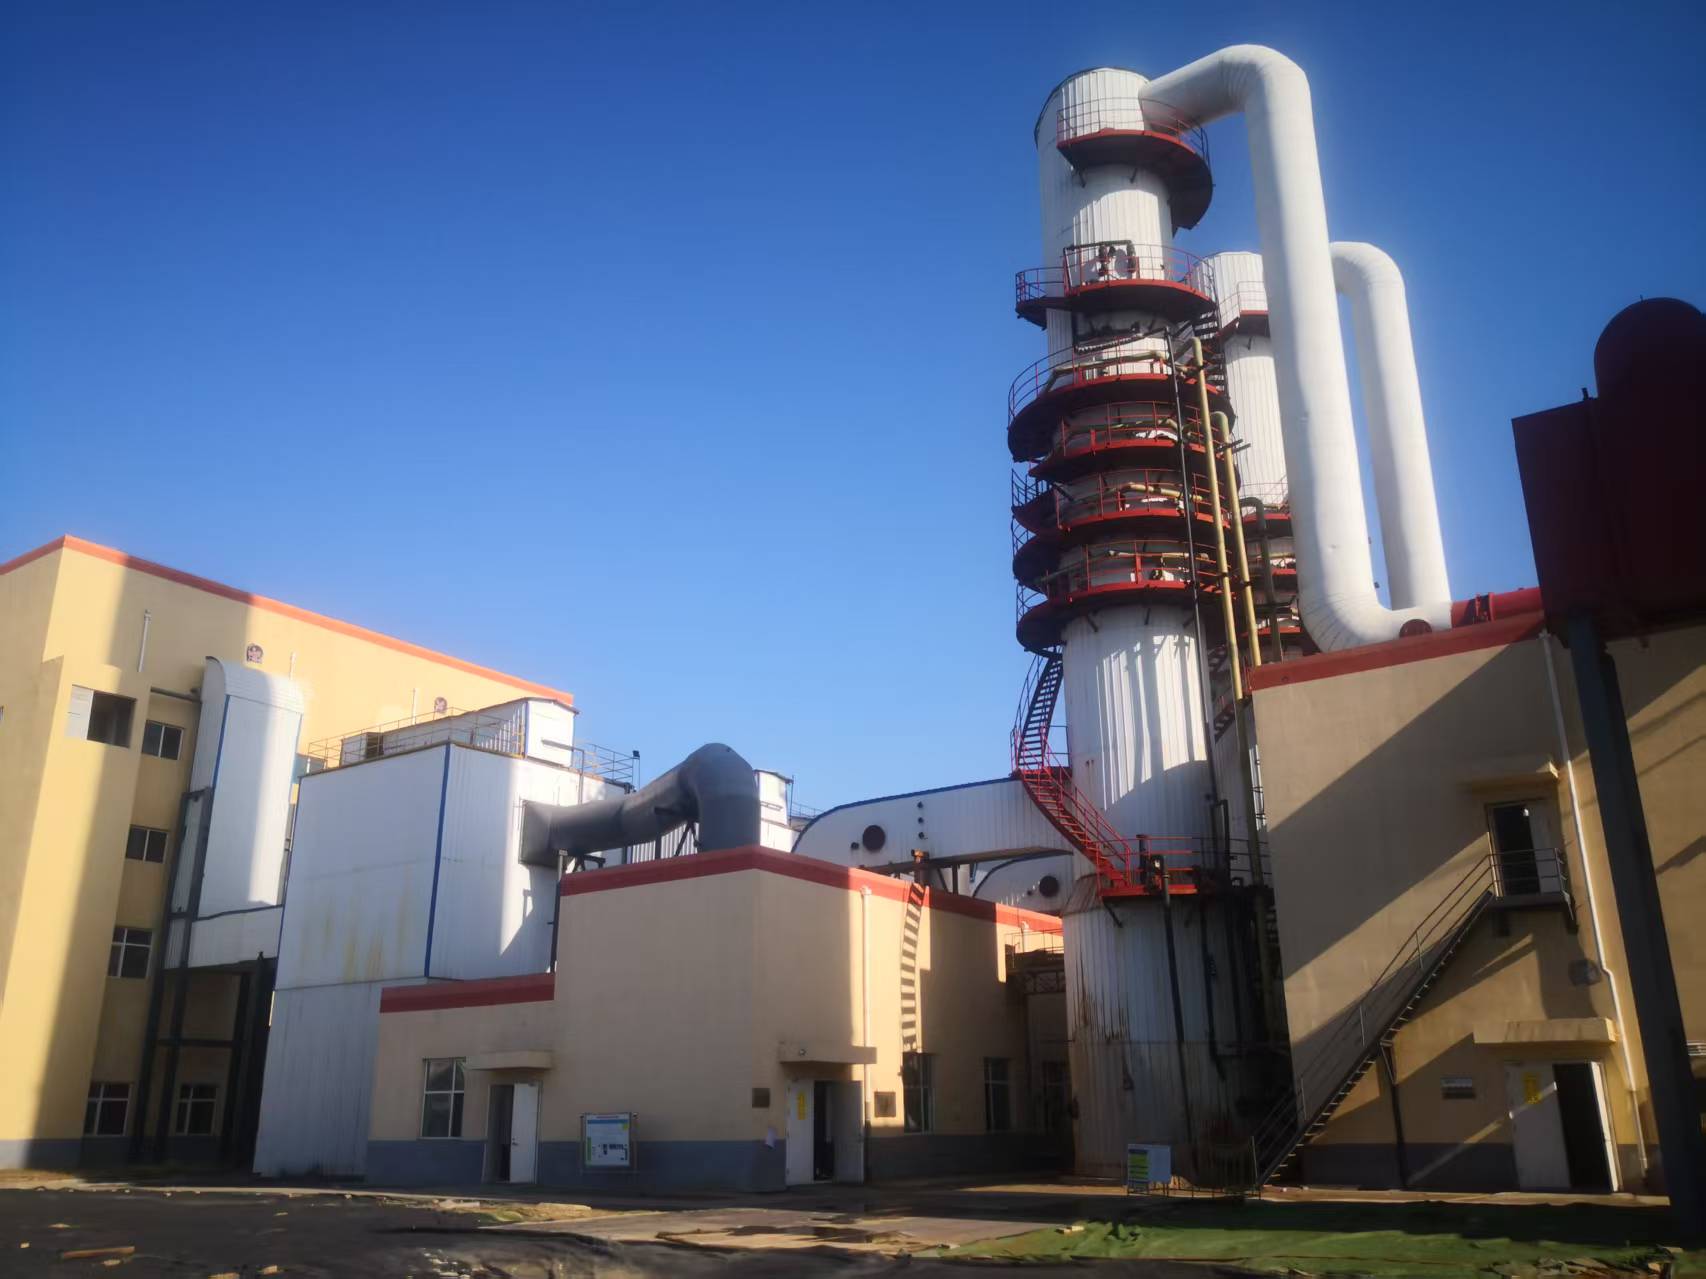
An industrial CFB boiler manufacturer specializes in producing Circulating Fluidized Bed boilers that represent cutting-edge thermal energy solutions for large-scale industrial operations. As a leading industrial CFB boiler manufacturer, these companies engineer systems designed to handle diverse fuel types while maintaining exceptional efficiency and environmental compliance. The industrial CFB boiler manufacturer develops boilers that utilize advanced fluidized bed technology, where fuel particles circulate within a hot sand bed, enabling complete combustion and superior heat transfer. Main functions include steam generation for power plants, chemical processing facilities, and manufacturing plants requiring reliable thermal energy. Technological features distinguish any professional industrial CFB boiler manufacturer through integrated automation systems, multi-fuel capability, and real-time monitoring technologies. These systems can efficiently burn coal, biomass, waste materials, and other fuels simultaneously, making them remarkably versatile. Applications span across power generation, district heating, industrial steam production, and energy recovery systems. An experienced industrial CFB boiler manufacturer incorporates advanced emission control technologies, ensuring compliance with stringent environmental regulations while maximizing operational efficiency. The design philosophy emphasizes reliability, scalability, and long-term cost-effectiveness. Modern industrial CFB boiler manufacturer offerings include modular configurations that accommodate various capacity requirements, from medium-scale operations to massive industrial complexes. These boilers operate at lower combustion temperatures compared to conventional pulverized coal boilers, reducing NOx emissions significantly. The industrial CFB boiler manufacturer continuously innovates, integrating digital controls, predictive maintenance features, and remote monitoring capabilities to optimize performance and minimize downtime throughout the boiler's operational lifespan.

New Product Recommendations

Selecting an experienced industrial CFB boiler manufacturer provides substantial operational and economic benefits that justify the investment for discerning industrial clients. Superior fuel flexibility stands as a primary advantage when partnering with a quality industrial CFB boiler manufacturer, allowing businesses to adapt fuel sources based on market availability and cost fluctuations. This adaptability ensures stable operating expenses and reduces vulnerability to fuel supply disruptions. Environmental compliance becomes effortless with an industrial CFB boiler manufacturer's advanced emission control systems, meeting strict regulatory standards without requiring expensive retrofitting. Lower NOx and SOx emissions protect the environment while eliminating potential regulatory fines. Enhanced combustion efficiency directly impacts operational costs, as industrial CFB boiler manufacturer systems extract maximum thermal energy from available fuel, translating to reduced fuel consumption and improved profitability. Scalability represents another compelling advantage, enabling facilities to expand capacity by adding modular units designed by an industrial CFB boiler manufacturer without complete system replacement. Extended equipment lifespan results from the industrial CFB boiler manufacturer's robust construction and lower operating temperatures, minimizing wear and extending maintenance intervals. Reduced maintenance requirements decrease labor costs and operational interruptions. Digital monitoring capabilities provided by progressive industrial CFB boiler manufacturer options enable real-time performance tracking, predictive diagnostics, and optimized energy distribution. Automation features streamline operations, reducing manual intervention and human error. Long-term reliability ensures consistent steam production supporting continuous manufacturing processes. Cost-effectiveness emerges through lower operational expenses, reduced environmental compliance costs, and minimal downtime. When evaluating boiler solutions, engaging an industrial CFB boiler manufacturer with proven expertise delivers measurable returns on investment, operational stability, and competitive advantages within energy-intensive industries.

Tips And Tricks

How does fluidized bed combustion adapt to sudden fuel composition shifts?

15

Sep

How does fluidized bed combustion adapt to sudden fuel composition shifts?

Fuel composition variability remains one of the most challenging operational parameters in modern thermal power generation. When feedstock sources shift unexpectedly or intentionally blend different materials, systems must respond quickly to maintain...
View More
What temperature range ensures optimal efficiency in fluidized bed combustion?

25

Sep

What temperature range ensures optimal efficiency in fluidized bed combustion?

Understanding the optimal temperature range for fluidized bed combustion is essential for operators seeking to maximize boiler performance and reduce operational costs. Temperature control directly influences combustion efficiency, fuel consumption r...
View More
How does a circulating fluidized bed optimize the combustion residence time?

22

Oct

How does a circulating fluidized bed optimize the combustion residence time?

The circulating fluidized bed represents a transformative approach to combustion optimization in industrial power generation. Unlike traditional fixed-bed systems, this technology maintains fuel particles in continuous suspension within the combustio...
View More
What prevents bed agglomeration inside a heavy-duty circulating fluidized bed?

29

Oct

What prevents bed agglomeration inside a heavy-duty circulating fluidized bed?

Bed agglomeration represents one of the most significant operational challenges in heavy-duty circulating fluidized bed systems, where fine particles and ash combine to form large, unfluidizable clusters that compromise combustion efficiency and equi...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial cfb boiler manufacturer

Advanced Multi-Fuel Combustion Capability

Advanced Multi-Fuel Combustion Capability

A premier industrial CFB boiler manufacturer delivers exceptional multi-fuel capability that transforms operational flexibility and cost management for industrial enterprises. This distinctive feature enables simultaneous combustion of coal, biomass, waste-derived fuels, and alternative energy sources within a single system. The industrial CFB boiler manufacturer's design accommodates fuel variability, allowing seamless transitions between available resources based on market pricing and supply chains. Organizations benefit from reduced fuel procurement dependencies while maintaining consistent steam output and operational continuity. The fluidized bed technology employed by an industrial CFB boiler manufacturer ensures complete fuel combustion regardless of fuel composition variations, optimizing thermal efficiency across different fuel types. This adaptability proves invaluable for facilities seeking energy independence and protection against volatile fossil fuel markets. The industrial CFB boiler manufacturer incorporates sophisticated fuel handling systems and combustion control mechanisms ensuring uniform energy extraction. Multi-fuel compatibility supported by an industrial CFB boiler manufacturer significantly reduces operational costs through opportunistic fuel sourcing strategies. Manufacturing plants, power generation facilities, and district heating systems gain substantial competitive advantages through this transformative capability.
Superior Environmental Performance and Regulatory Compliance

Superior Environmental Performance and Regulatory Compliance

An innovative industrial CFB boiler manufacturer prioritizes environmental stewardship through advanced emission control technologies that significantly exceed regulatory requirements. The industrial CFB boiler manufacturer's systems operate at lower combustion temperatures, naturally reducing NOx formation compared to conventional boiler designs. Advanced air staging, limestone injection, and integrated scrubbing systems deployed by an industrial CFB boiler manufacturer effectively minimize SO2, NOx, and particulate emissions. Facilities partnering with an industrial CFB boiler manufacturer achieve effortless compliance with progressively stringent environmental regulations, eliminating costly retrofitting and potential penalties. The industrial CFB boiler manufacturer's commitment to sustainability supports corporate environmental objectives while protecting community air quality. Real-world deployment demonstrates that industrial CFB boiler manufacturer solutions consistently exceed compliance standards, providing regulatory confidence and operational peace of mind. Environmental certification achievement becomes straightforward when utilizing systems from an industrial CFB boiler manufacturer, enhancing corporate reputation and stakeholder relationships. Comprehensive emission monitoring capabilities provided by an industrial CFB boiler manufacturer enable transparent environmental reporting. Investment in industrial CFB boiler manufacturer technology represents genuine environmental commitment while maintaining profitability and competitiveness.
Intelligent Automation and Remote Diagnostic Systems

Intelligent Automation and Remote Diagnostic Systems

Leading industrial CFB boiler manufacturer offerings integrate sophisticated automation and diagnostic technologies that revolutionize operational management and maintenance efficiency. Modern industrial CFB boiler manufacturer systems feature advanced control algorithms monitoring combustion parameters, fuel feed rates, and system pressure continuously throughout operation. Real-time diagnostic capabilities embedded within industrial CFB boiler manufacturer technology identify potential issues before they escalate into costly failures, enabling proactive maintenance scheduling. Remote monitoring capabilities allow an industrial CFB boiler manufacturer's support teams and facility operators to access performance data from anywhere, ensuring rapid response to anomalies. Predictive maintenance algorithms supported by industrial CFB boiler manufacturer platforms optimize replacement scheduling, reducing unexpected downtime significantly. Automated optimization routines executed by an industrial CFB boiler manufacturer's systems maximize thermal efficiency automatically, adapting to changing operating conditions instantaneously. Performance analytics provided by an industrial CFB boiler manufacturer facilitate data-driven operational decisions and continuous improvement initiatives. Integration capabilities allow industrial CFB boiler manufacturer systems to communicate with broader facility management infrastructure, enabling coordinated energy optimization strategies. Staff training requirements decrease substantially with automated functions provided by industrial CFB boiler manufacturer solutions, reducing operational complexity and improving safety. Digital innovation delivered by industrial CFB boiler manufacturer technology represents genuine advancement in boiler system management.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
email goToTop